
Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
Nullam dignissim, ante scelerisque the is euismod fermentum odio sem semper the is erat, a feugiat leo urna eget eros. Duis Aenean a imperdiet risus.
A STOP button sits at the front line of machine safety. On a lawn mower or outdoor power equipment, it is the part an operator hits – hard, fast, sometimes with gloves on – to cut power in an emergency. That single part has to survive years of sunlight and rain, take repeated impacts without cracking, keep its bright red identification legible, and still click into the housing with a precise, positive feel. Few parts combine outdoor weathering, impact duty and visible appearance in one molded piece the way a safety button does.
In this case we manufactured a custom STOP button in ASA (acrylonitrile styrene acrylate) for outdoor power equipment, covering mold development, precision injection molding, and mass production with inspection and packing. The sections below explain the material choice, the molding considerations behind the ribbed back structure, and how the parts are fitted and checked.
Outdoor equipment lives outdoors in every sense: direct UV exposure, rain, temperature swings and dust. General-purpose ABS would chalk and fade within seasons; ASA was engineered for exactly this gap. It offers outstanding UV resistance and weather stability, so the red color of this button stays vivid and the surface stays intact even after long exposure – which matters here, because a faded stop control is a safety problem, not just a cosmetic one.
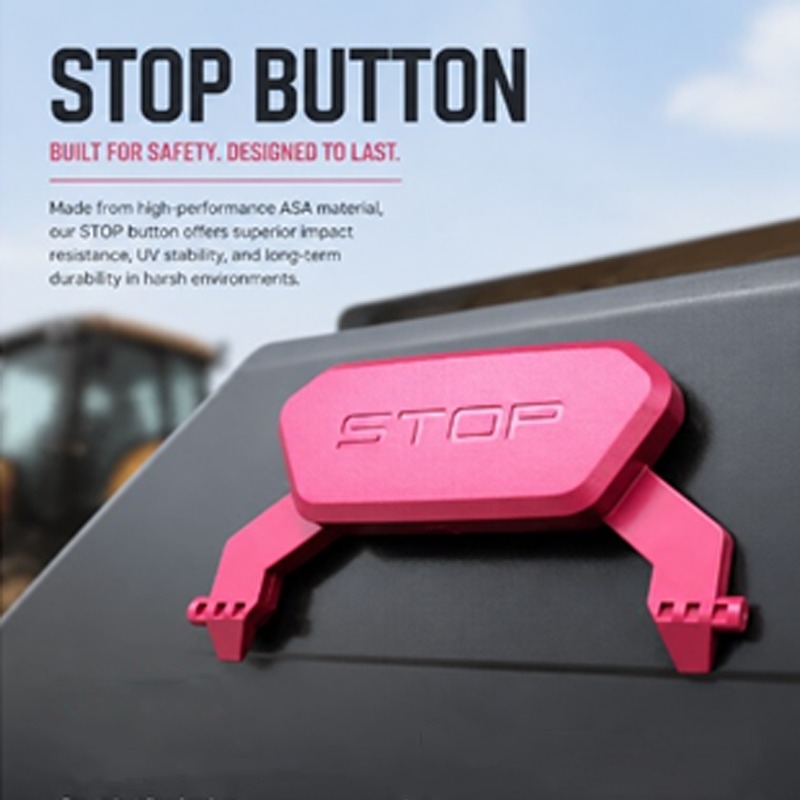
ASA also brings the impact resistance and rigidity the button needs for its duty cycle. Operators press it hard, sometimes in cold weather when plastics are at their most brittle; the ASA grade selected for this part keeps enough toughness year-round. The material machines and molds into crisp edges, which is what allows the raised STOP marking to be molded directly into the surface – sharp, legible, and impossible to peel or wear off the way a printed label would.
The button’s visible face is completely flat and glossy, which means every molding flaw shows: flow marks, sink over the internal ribs, gate blush, weld lines. The mold was gated so the flow front crosses the face evenly, polished to a uniform finish, and vented at the far edges to prevent burns. Holding pressure and cycle were tuned until the ribbed back packed out fully without telegraphing sink through the front face.
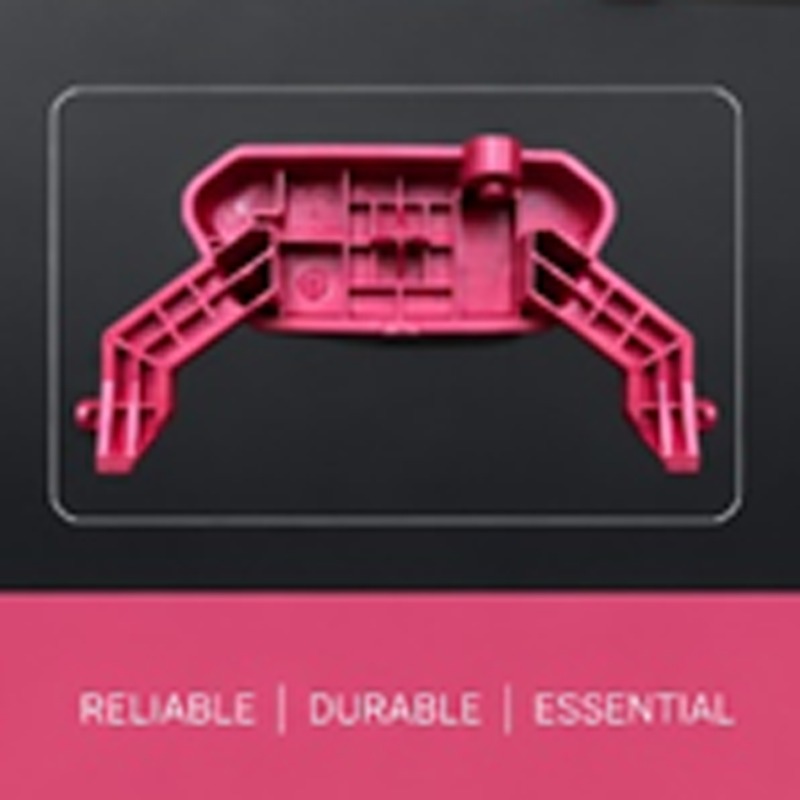
Turn the button over and the reason it survives hard use becomes visible: a dense grid of internal ribs braces the large flat face against bending, and the two curved mounting legs are ribbed as well, so the snap-in legs flex during assembly but resist fatigue over years of service. All of these ribs are molded in one shot – their thickness was optimized in DFM so they add rigidity without creating sink on the opposite face.
During trials the button was fitted to the actual housing: the legs were checked for insertion force and retention, the contact points for interference, and the button face for flush seating against the panel. After repeated press-release cycles, the legs and the molded STOP marking showed no whitening or wear – the practical standard for a part whose job is to keep working after years of emergency use.
Looking for a manufacturing partner for your safety control components or other outdoor plastic parts? Send us your drawing or sample – Kunshan Maifeng Precision provides product structure review, custom mold design and manufacturing, single- and dual-color injection molding and product assembly, and we will be glad to quote your project from mold development to mass production.

Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². Our manufacturing resources include 36 single- and dual-color injection molding machines from 90 to 700 tons and more than 50 sets of mold manufacturing and processing equipment. Supported by a service, management and production team of over 100 people, we provide product design, mold design and manufacturing, injection molding, and product assembly. Our parent company was established in 2008.
1. Product Design
Product structure design and optimization based on customer drawings and samples.
2. Mold Design
Mold concepts developed around product requirements, material and production needs.
3. Mold Manufacturing
Machining, polishing, assembly and related processes for custom molds.
4. Injection Molding
Single- and dual-color molding capabilities for custom production.
5. Product Assembly








 English
 Chinese