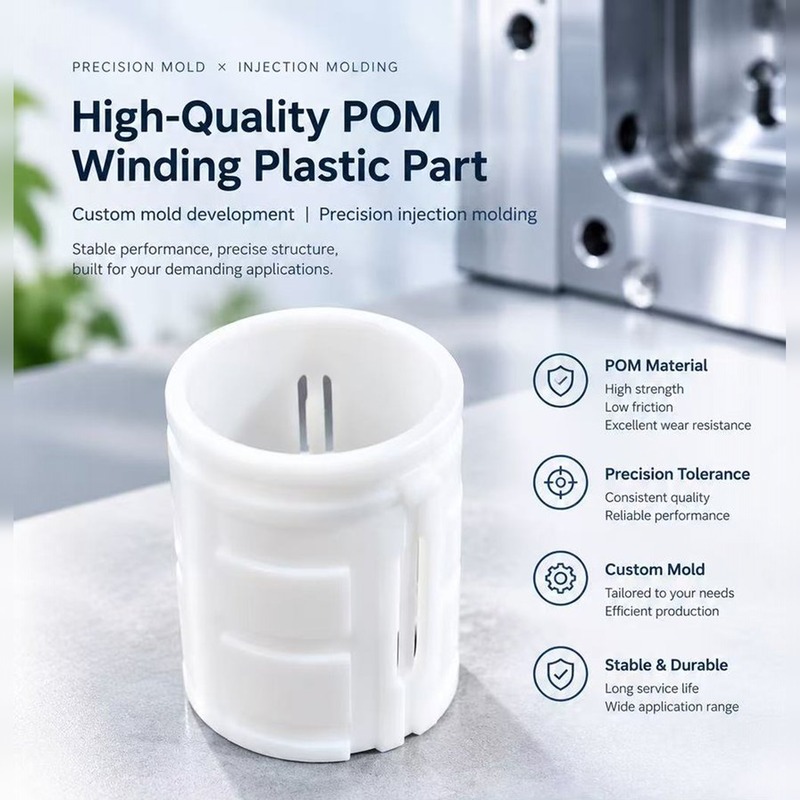
This is a small part that has to stay round. It is a white POM winding component: a thin cylindrical wall, a set of functional ribs around the outside, axial slots cut through the wall, and two open ends that both have to hold their diameter after the part leaves the tool. Where it is used, something winds onto it or runs against it, and any ovality, taper or wall-thickness drift turns into wobble, noise or wear at the mating part.
It is molded in POM for the reasons the material is chosen in this kind of duty: stiffness, low friction, wear resistance and dimensional stability in humid air. But POM is also one of the less forgiving resins to tool, and most of this page is about that — how the wall, the ribs and the slots are laid out, how the core and the ejection are built, what is measured at the machine, and how the parts are packed so that a full carton arrives as round as the sample that was approved.
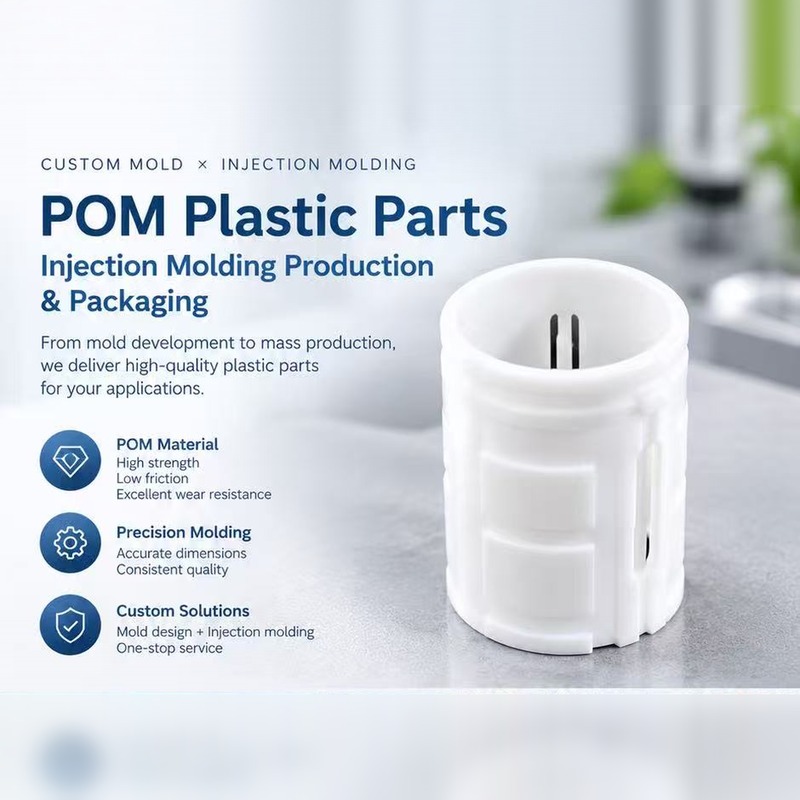
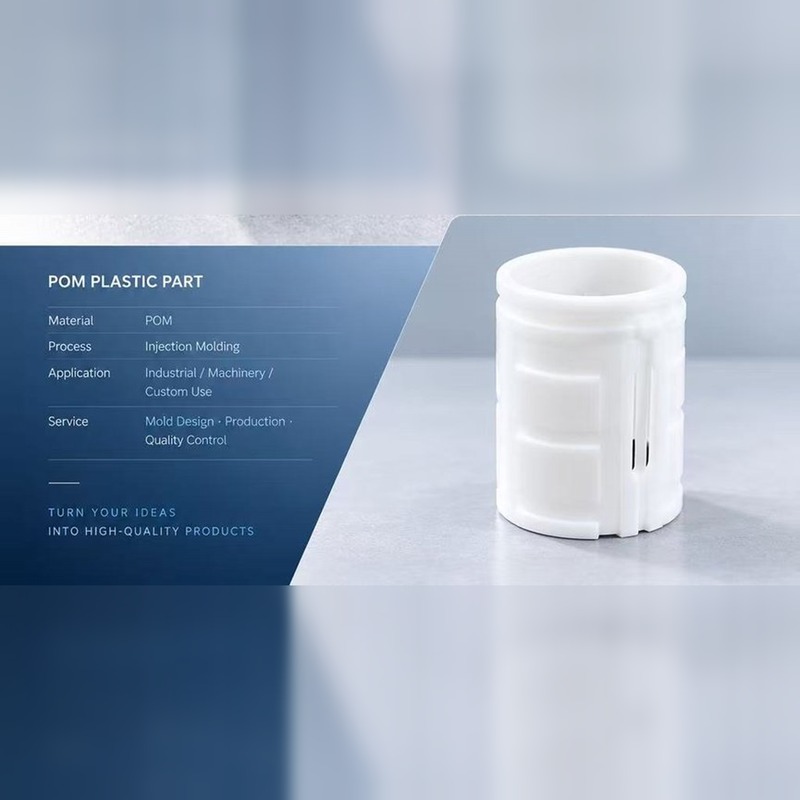
The part: a thin cylindrical wall, functional ribs on the outside, and slots cut through the wall at the open end.
Why POM, and What It Costs You
POM brings three properties to a part like this that no commodity plastic matches at the same price. It is stiff enough that a thin cylindrical wall keeps its shape under load instead of breathing. It has a low coefficient of friction against itself and against metal, so a surface that slides or rotates runs cool and quiet. And it wears slowly and predictably, which is why it is the default for small gears, bushings, rollers and winding bodies. It also holds its dimensions in humid air far better than nylon, which matters for a part whose fit is measured in hundredths of a millimetre.
The costs are worth stating before a tool is cut. POM shrinks a lot — on the order of two percent, and unevenly between wall sections, so a thick rib next to a thin wall pulls the round body out of round. It has a sharp melting point and a narrow process window: run it cold and the weld line where the melt fronts meet stays weak and visible, run it hot and it can degrade and give off formaldehyde. It does not bond well, so no glued insert or stuck-on label should be part of the design. And it is not a hot-water or steam material — if the part has to be sterilized in an autoclave, this is the wrong resin and the conversation should happen before the drawing is frozen, not after.
The Wall, the Ribs and the Slots
The body is a tube, and a tube is a cooling problem before it is anything else. Wall thickness is held uniform around the full circumference, because every place where it is not becomes a shrink gradient, and a shrink gradient on a cylinder is ovality. The ribs on the outside are there for two reasons: they stiffen the wall against the squeeze of a winding load, and they give an assembly fixture or a hand something to key against. Each rib is drafted and filleted at its root, and the root thickness is kept to roughly half the wall so the rib does not sink a flat onto the inside bore — on a white part, a sink on the bore reads immediately under a light.
The slots are the harder feature. They are cut through the wall, so the melt has to flow around them, and the two flow fronts that meet on the far side of each slot leave a weld line. Where that weld line lands decides how the part fails: put it at a slot edge and the edge chips when the part is loaded; put it in a plain wall section and it is a cosmetic line that a customer will accept. Gate position is chosen for that, not for convenience. Slot width and position are formed by inserts in the cavity, so they can be changed later without cutting a new tool body, which is usually the cheapest way to accommodate a design revision.
One part, one tool, one process window: mold development and molding are held together so the geometry does not drift between lots.
Tooling: Core, Ejection and Concentricity
A deep, thin tube needs a long core, and a long core is where roundness is won or lost. The core is ground and polished along its full length, drafted enough to release without scuffing but not so much that the bore tapers beyond tolerance, and cooled from the inside — a core that runs hot at its tip gives a bore that is tight at one end and loose at the other, and no amount of tweaking at the machine fixes it. Concentricity between the bore and the outside diameter is a tool alignment item: core and cavity have to share a centre, and that is checked on the first shot rather than assumed.
Ejection is the other place a thin wall shows damage. Pins pushing on a two-millimetre wall leave witness marks and can dome the end face; this tool ejects on a stripper sleeve that pushes the full end face at once, so the load is spread around the rim. Where a pin ejection is unavoidable, the pins sit on the rib roots rather than on plain wall, because that is where the section is thickest and the mark is least visible.
From the Machine to the Inspection Bin
Parts come out of the tool on a fixed cycle, are taken out by the robot at the top of the stroke, and drop into a bag-lined bin at the machine rather than onto a conveyor or into a loose carton. That choice is deliberate: a POM part with a thin wall that lands on another part can pick up a nick on the bore lip, and a nicked lip is a fit problem at the customer’s assembly station that nobody can trace back to the molding room.
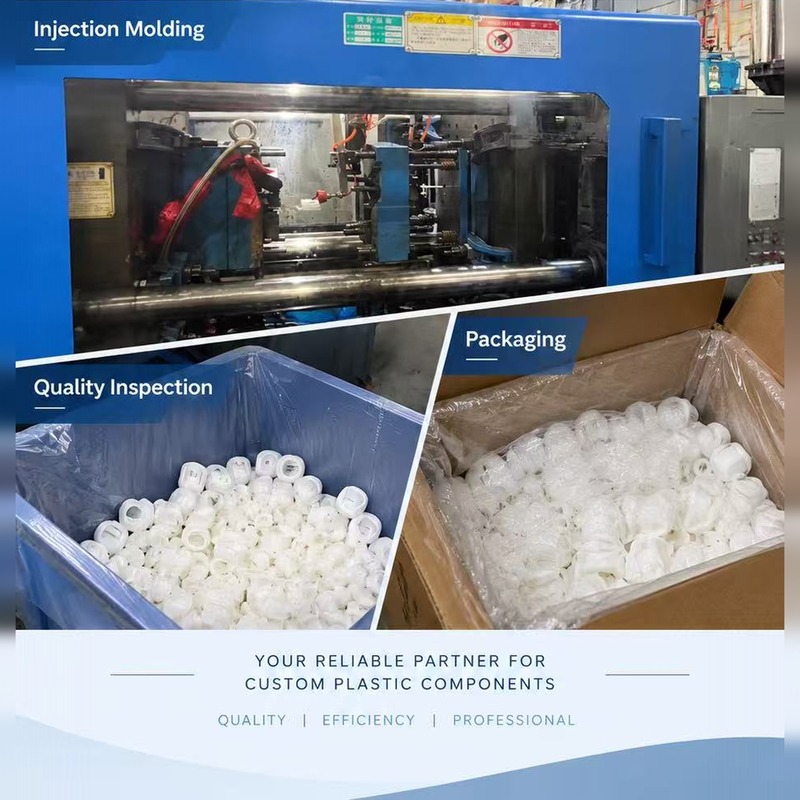
The tool running, the robot take-out at the top of the stroke, and the finished white parts collected in the bag-lined bin at the machine.
Molding conditions are locked once the first-article parts pass, and the parameters that matter for this geometry are the ones that control shrink: hold pressure and hold time, melt temperature, and mold temperature on both halves. A drift in mold temperature of a few degrees is enough to move the bore diameter outside its band, so the temperature controllers are on the daily check sheet along with the machine parameters.
What Is Checked Before the Parts Are Packed
Inspection for a part like this is dimensional first and cosmetic second, and it is done on a sampling plan tied to the lot rather than on a single part at the start of the run.
Outside diameter and bore diameter, measured at both ends of the part, not just the middle — a taper shows up nowhere else.
Roundness of the bore and the outside diameter, checked against the drawing’s tolerance band.
Wall thickness at several points around the circumference, which is the fastest way to catch a core that has shifted.
Slot width, slot position and slot edge condition, since a chipped edge fails a fit even when every dimension is inside tolerance.
Overall length, rib profile and rib root condition.
Appearance under a raking light: short shots at the slot edges, sink opposite a rib, flash on the end faces, and colour against the approved master.
Packing follows the same logic. Parts are counted by weight against a counted sample, bagged in a liner inside a carton so that they cannot shift in transit, and the carton is marked with the lot, the cavity count and the date. Bulk packing is fine for a part this size; what is not fine is a carton that arrives with the parts crushed against each other, because the damage is invisible until the customer’s assembly fixture rejects the first one.
What Can Be Customized
The tool is built around your drawing, so almost every feature on this part is a variable rather than a fixed item: the bore and outside diameter, the wall thickness, the number and position of the ribs, the slot width and length, the end-face geometry, and the colour. Material grade is a variable too — standard POM copolymer for general duty, a higher-stiffness grade where the wall has to carry more load, or a wear-modified grade where the part runs against metal at speed.
The short version: POM, injection molded, industrial or machinery duty — with mold design, production and quality control handled in house.
Cavity count is a commercial decision as much as a technical one. A single-cavity tool is the cheapest way to start and the right answer for a low volume or a design that is still moving; a multi-cavity tool pays for itself on a stable annual volume, but it also multiplies every tolerance in the tool, so the cavity layout and the cooling are designed together from the first sketch. If the volume is uncertain, we usually recommend starting single or two-cavity and building the second tool when the demand is proven.
The three stages on one page: molding at the machine, inspection from the bin, and packing for shipment.
Information to Confirm Before Starting a POM Part Project
The part drawing with tolerances on bore, outside diameter, roundness, wall thickness and slot position, and a note on which of them are functional.
What the part does — what winds onto it, what it slides against, and at what speed and load — because that decides the POM grade and the wear allowance.
Any temperature, chemical or cleaning exposure in service, so an unsuitable resin is ruled out before the tool is cut.
Colour and appearance standard, including whether a weld line in a plain wall section is acceptable.
Annual volume and the expected life of the program, which set the cavity count and the tool steel.
Packing and labeling requirements, and whether parts ship bulk, in trays, or as kits.
Kunshan Maifeng Precision Industry Co., Ltd. reviews the drawing and the application before quoting, builds the injection mold in house, molds POM on 36 machines from 40 to 700 tons, and inspects and packs to the drawing and the carton specification. Send us a drawing or a sample with the tolerances that actually matter, and we will come back with a tooling proposal, a material comment and a checking plan.
Contact Us
Lucy Liu — Kunshan Maifeng Precision Industry Co., Ltd.
Phone / WhatsApp: +86 17714686855
Custom Mold. Precision Injection Molding. Reliable Production. Let us help turn your plastic component design into a high-quality manufactured product.
Company Profile
About Us
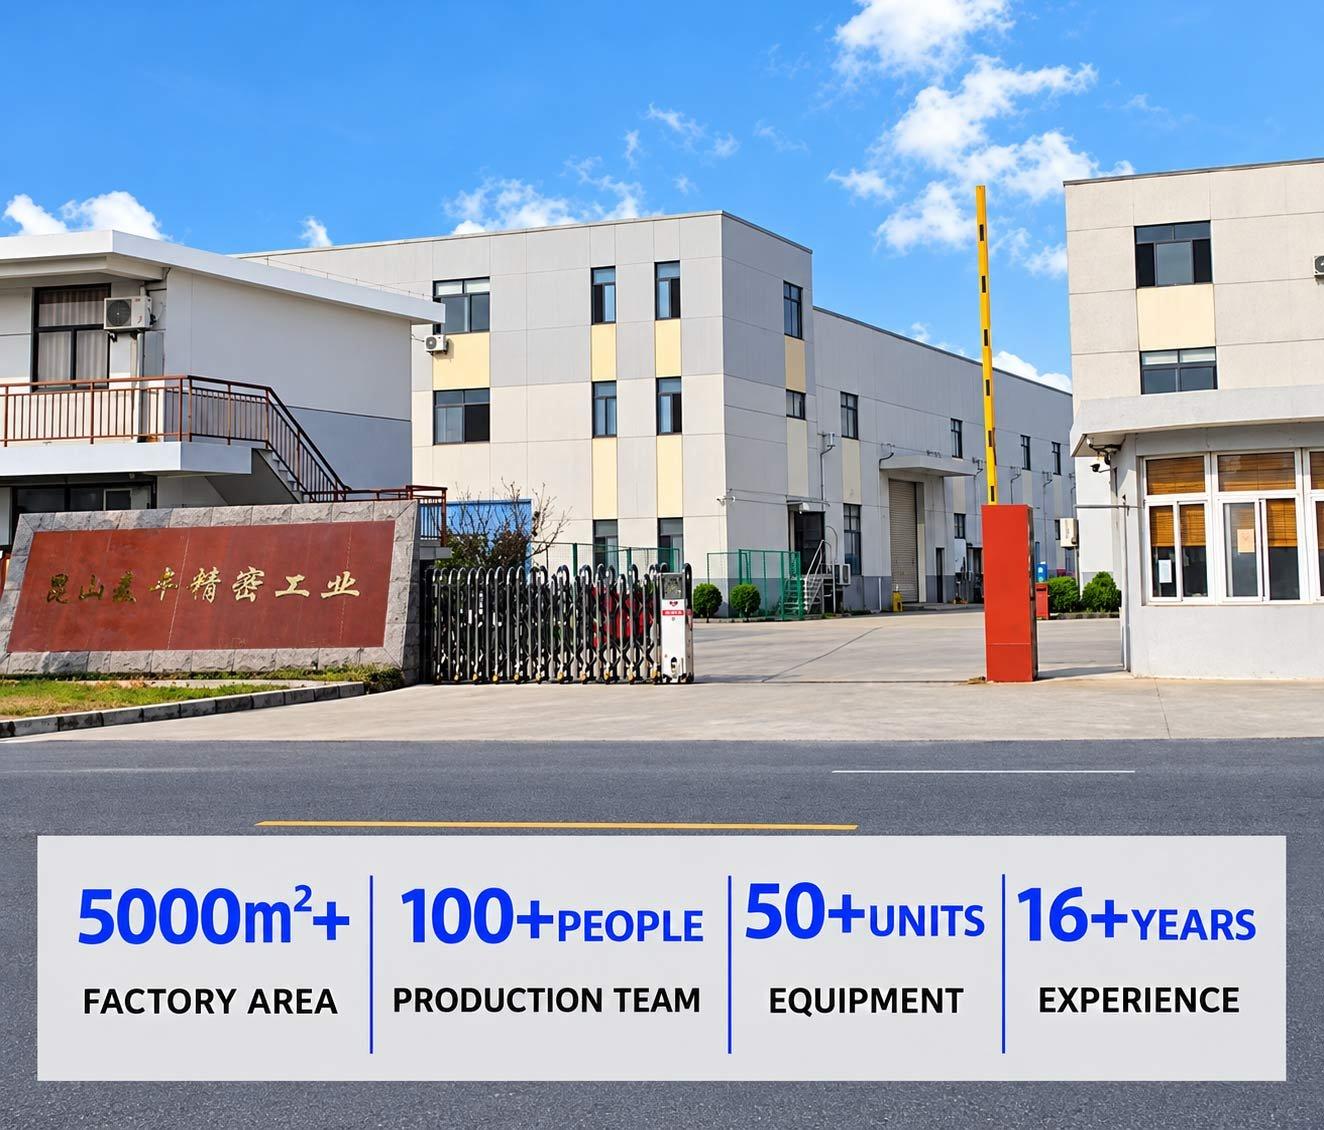
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 40 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design
Product structure design and optimization based on customer drawings and samples.
2. Mold Design
Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing
Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding
Single- and dual-color injection molding for project and order requirements.
5. Product Assembly
Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.











 English
 Chinese



