Lawn Mower Protective Decorative Cover, Glossy Black PC Injection Molded
Glossy black PC protective and decorative cover for lawn mowers, molded with formed snap clips, a ribbed inner face and a class-A outer surface, then inspected for flow marks, ring roundness and clip force before packing.
Open-ring PC shell molded in one shot, with the snap clips and locating tabs formed by slides instead of assembled afterwards.
Class-A gloss black face polished in one direction and gated on a hidden edge, so no flow mark, sink or gate witness lands where the customer looks.
A protective cover on an outdoor machine has two jobs that are usually given to two different parts: it has to shield something behind it, and it has to look like it belongs on a machine that costs more than a car. On a mower, that means a glossy black shell that takes a knock from a stone or a kerb, hides the mechanism underneath, and still reads as a clean line against the bodywork.
This page is about the part in the photos — an open-ring PC cover with a class-A gloss black outer face, a ribbed inner face and a set of clips that hold it on without a single screw. It is molded in one shot, and the engineering sits in three places: keeping the outer face free of flow marks and sink, holding the open ring round so it snaps on and stays on, and forming the clips with slides instead of assembling them afterwards.
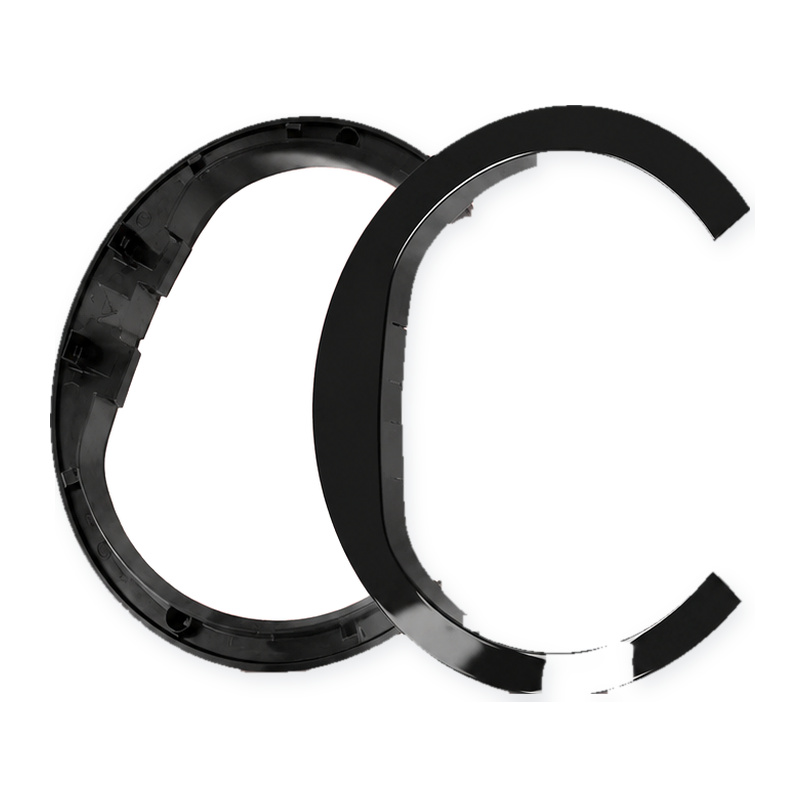
The cover as it comes off the tool: a glossy black PC shell with the clip details formed on the inner face.
What This Cover Is For
The part is a three-quarter ring, not a closed circle. The opening at the front is deliberate: it lets the cover slide over the component it protects and flex enough to clip on, and it leaves a gap where the machine’s own geometry comes through. Around the inside face there are ribs, locating tabs and two latch details; the outside is a continuous high-gloss surface that the customer sees every time they walk past the machine.
Because it is both a guard and a visible trim part, the acceptance criteria come from two directions at once. From the functional side: does it clip on with a defined push force, does it stay on through vibration, does it protect the part underneath from a hit. From the cosmetic side: no flow mark, no weld line on the lit face, no sink opposite the ribs, no gate witness on a visible surface, and a gloss level that matches the rest of the machine’s plastics after two years in the sun.
Two parts from the same tool: the gloss face on one side, the ribs, tabs and clip details on the other.
Why PC, and Why Gloss Black Is the Hard Part
Polycarbonate is the natural choice for a part that is expected to be hit. It absorbs impact that would crack a styrenic cover, it holds its shape at the temperatures a mower deck reaches in direct sun, and with UV stabilization it keeps both its colour and its gloss outdoors. A PPE or ABS cover would be cheaper per kilo and would look identical in the showroom — and then crack the first winter.
The material is not the difficult part. The gloss is. A class-A black surface shows everything the tool and the process do to it, in this order of visibility:
Flow marks and weld lines — black gloss reflects like a mirror, so any change in surface orientation shows as a shift in the reflection. Weld lines have to be pushed to a hidden edge or into the rib side, which is a gate-position decision, not a polishing decision.
Sink opposite the ribs — every internal rib pulls material away from the outer face as it cools. Rib thickness is kept to roughly half the wall, and the pack pressure and cooling time are set so the face stays flat.
Gate witness — a gate on a visible gloss face is a permanent defect. The gate is placed on a hidden edge, inside the clip pocket, or on a tab that is trimmed and touched up.
Polish direction — the cavity is polished in one direction and to a defined grade. A patch that is polished differently reads as a dull spot under a low sun, which is exactly when the customer inspects it.
All of that is decided before the cavity block is finished. A gloss tool that is polished “as well as possible” cannot be rescued by process settings afterwards.
Gloss black PC: impact resistance, heat resistance and a surface that has to survive being looked at closely.
An Open Ring Has to Keep Its Shape
An open ring is the least forgiving shape to mold flat. The moment the part is pushed off the core it wants to relax: the opening either closes or springs wider, the ring goes oval, and the clips that were designed to a tenth of a millimetre no longer line up with the feature they grip.
Three things control it, and only one of them is in the tool:
Even cooling on both faces. A gloss face and a ribbed face cool at different rates; if the difference is large the part curls towards the gloss side. Cooling channels follow the ring rather than sitting in straight lines across the block.
Ejection on structure. Ejector pins land on the rib side and on the end faces, never on the gloss wall, and they push together rather than one side first.
Rest, not bin. Parts come out warm and are laid on a shaped rest to cool in the geometry they were molded in. A cover that is tipped into a carton while still soft is a cover that will not fit.
The check is a fixture, not an eye. The ring is placed on a gauge cut to the drawing, the opening is measured across the two ends, and the clip positions are checked against the mating part. Where the customer assembles by hand, we also measure the push-on and pull-off force on a sample, because “it clicks” is not a specification.
The Clips Do the Work
Every latch on this cover is an undercut. That means the tool has to release it: either a slider travelling sideways, a lifter, or a collapsible core detail, and each one of those leaves a witness line where it meets the rest of the cavity. The design question is not whether to use a slide, but where to put the witness so it lands out of sight — usually on the inner face or on a surface the machine covers.
Snap details also set the material behaviour. A clip that is too stiff will not go on by hand; a clip that is too soft will rattle off on the first bumpy lawn. Wall thickness at the snap, the radius at its root, and the amount of interference are decided together, and then proven on a first article with a force gauge rather than assumed from the model.
The tool that makes it: a circular cavity on a four-pillar base, with the slides that free the latch details.
From the Press to the Carton
PC is dried before it is molded — around 120 °C for four hours — because moisture in the melt turns into silver streaks, and on a black gloss face a silver streak is not a small defect. The part is then taken out by the frame, not by the gloss wall, and laid on a rest. The video below is the actual line: the tool cycling, the robot taking the cover out, and the cover landing on the conveyor.
Molding the cover: the press cycle, the robot take-out by the frame, and the finished part on the line before packing.
Packing is where gloss parts are usually damaged. Covers are stacked with a soft liner between them or nested in a moulded tray so the gloss faces never touch, and they are shipped in a carton that can be opened at the assembly line without a knife near the parts. Where the customer’s line runs an automated feed, the tray pitch is agreed with them before the packaging drawing is released.
What Is Checked Before the Cover Is Packed
Gloss and colour — measured against a retained master under D65 light, on the face the customer sees; a gloss meter reading is recorded for the first article and the master is kept for re-orders.
Surface defects — flow marks, weld lines, silver streaks, scratches, gate witness and any polish patch, checked under a strip light at a low angle rather than straight on.
Ring roundness — the opening measured across the two ends on a fixture, plus the clip positions against the mating part.
Clip force — push-on and pull-off force on a sample from each shift, because this is the property that decides whether the part stays on the machine.
Wall and ribs — thickness at agreed points, and no sink visible on the gloss face opposite the ribs.
Fit trial — a first-article assembly on the customer’s component where the tool allows it, since a cover that measures well can still refuse to seat on a real machine.
What Can Be Customized
Geometry — arc angle, radius, width and end treatment, taken from the customer’s 3D model or from a scan of the part it has to cover.
Material and finish — PC in gloss, matte or fine-texture finish, UV stabilized for outdoor use; PC/ABS or ABS where the impact requirement is lower and the cost target tighter.
Colour — gloss black as standard, but any colour matched to a chip, a Pantone reference or a physical sample, with the master retained.
Fixing method — clips, snap tabs, screw bosses or a combination, designed around the housing that exists rather than the one that would be convenient.
Graphics and texture — a fine grain, a logo or a texture patch on the gloss face, cut into the cavity as a detail and polished around it.
Cavity count and packaging — single cavity for a low-volume machine, multi-cavity with a tray pitched for the customer’s assembly robot.
Information to Confirm Before Starting a Cover Project
3D model and drawing of the cover, plus the component it clips onto, so the clip positions and the ring opening can be checked against something real.
Gloss requirement — a gloss level or a reference part, and which surfaces are class-A and which are hidden.
Impact and environment — what hits the part, what it is cleaned with, and any outdoor power equipment standard or UV test it has to pass.
Assembly method — by hand, by robot, or with a jig; this decides the clip force window and the packaging format.
Colour standard — a chip or a physical sample, and the light source it will be judged under.
Annual volume and packaging — which decides cavity count, tray design and whether automation at the customer’s line is worth designing for.
Kunshan Maifeng Precision Industry Co., Ltd. reviews the drawing and the gloss requirement before quoting, builds the injection mold in house, and molds PC on 36 machines from 40 to 700 tons. Send us the 3D model of the cover with the mating part, and we will come back with a feasibility comment, a tooling proposal and the inspection plan we would run on the first article.
Parts from the same machine platform: a PC light diffusion tail light grille and a clear PC tail light strip, both molded to the same standard as this cover.
Contact Us
Lucie — Kunshan Maifeng Precision Industry Co., Ltd.
Custom Mold • Precision Injection Molding • Consistent Production. Send us the 3D model of the cover and the gloss requirement, and we will come back with a tooling proposal.
Company Profile
About Us
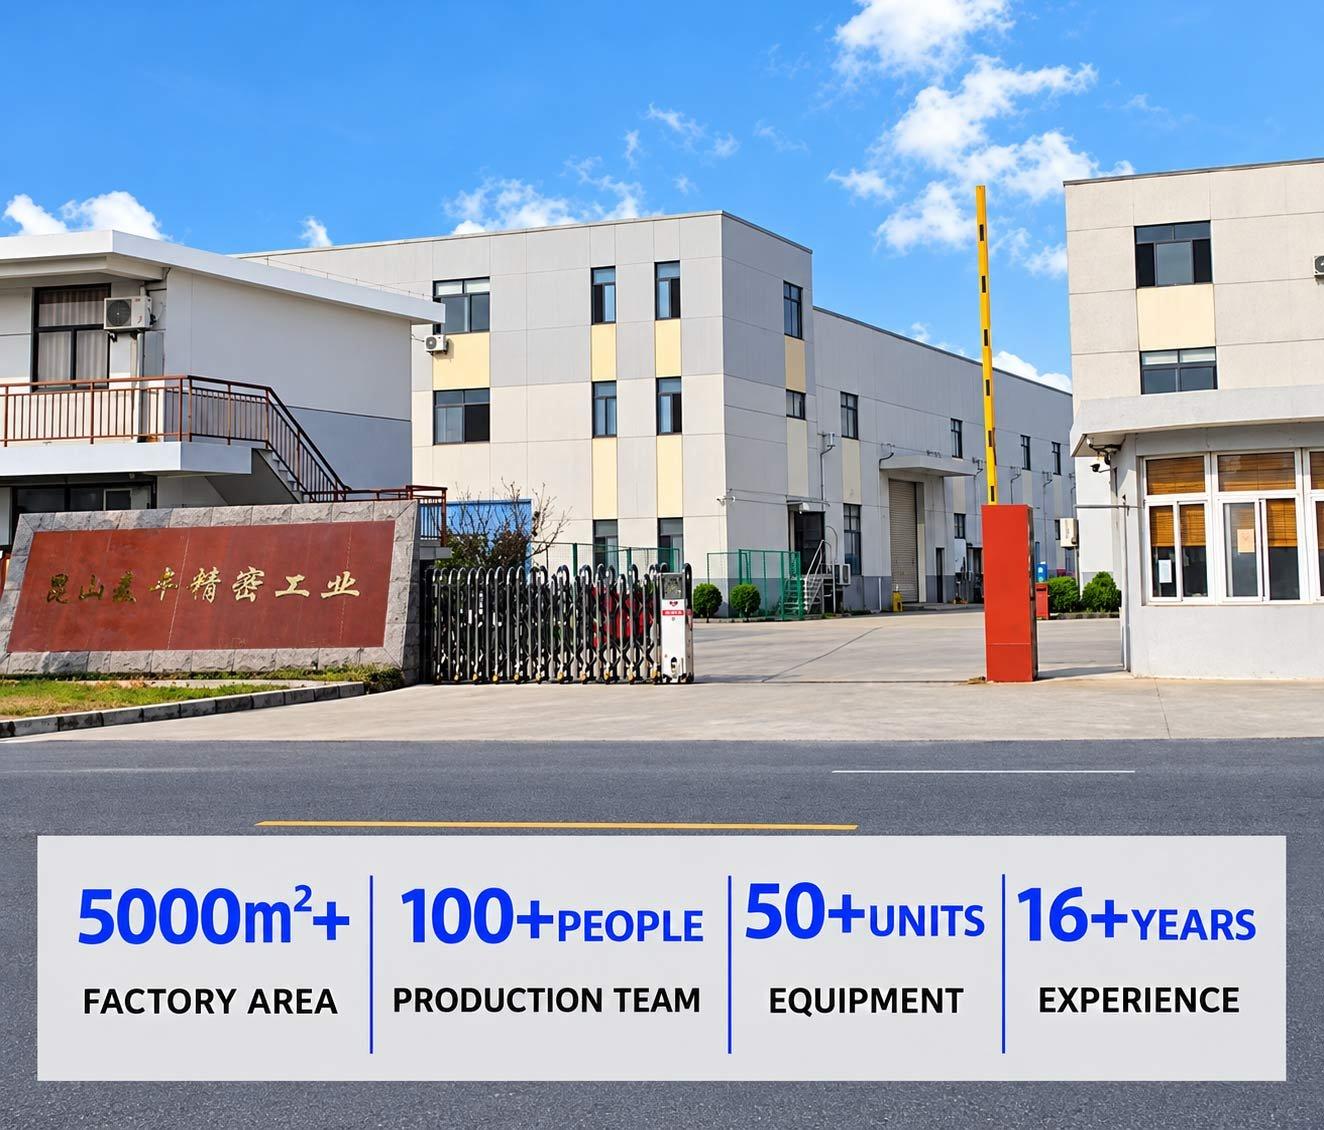
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 40 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.











 English
 Chinese



