This special-purpose knob for disposable electric linear cutting staplers is injection molded in one piece from a medical-grade resin. The flared body gives the fingers a rolling grip, with scalloped recesses at the wide end sized for gloved operation. The internal thread stack under the skirt converts finger rotation into the closing stroke and is cut in register with the outer profile, so the knob turns without wobble. Clip and guide features inside the skirt snap onto the operating mechanism at first assembly. Thread form, recess geometry and clip positions are built to the instrument mechanism drawing and verified with the mating parts.
internal thread cut in register with the outer profile, so rotation stays true without wobble
finger recesses sized for gloved hands, checked against glove geometry not a bare thumb
clip features built to the mechanism drawing and verified with real mating parts
The adjustment knob on a disposable stapler is turned a few times and thrown away with the instrument, but within those few turns it carries the whole closing stroke of the device. The surgeon’s fingers read its shape without looking, the internal thread converts their grip into precise travel, and the clip features underneath have to line up with the mating mechanism on the first assembly, every time.
The knob shown here is moulded in one piece from a light medical-grade resin in a flared, trumpet-like form. The photographs cover it from four angles including the underside, which carries the thread stack and the internal features that mate with the instrument body.
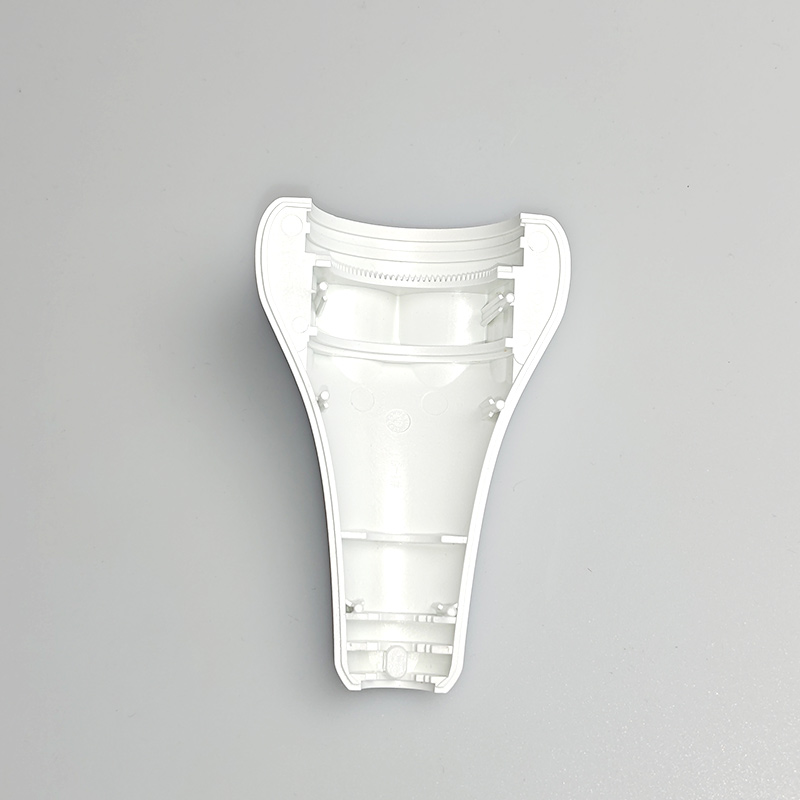
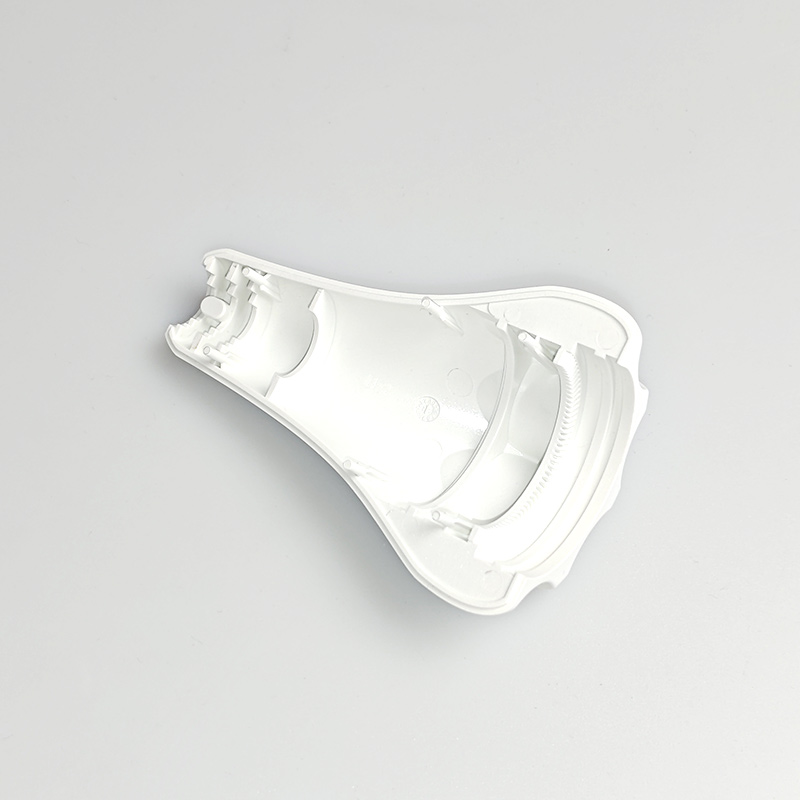
The underside. The internal thread stack converts finger rotation into the closing stroke of the instrument.
A Flared Body Moulds Differently
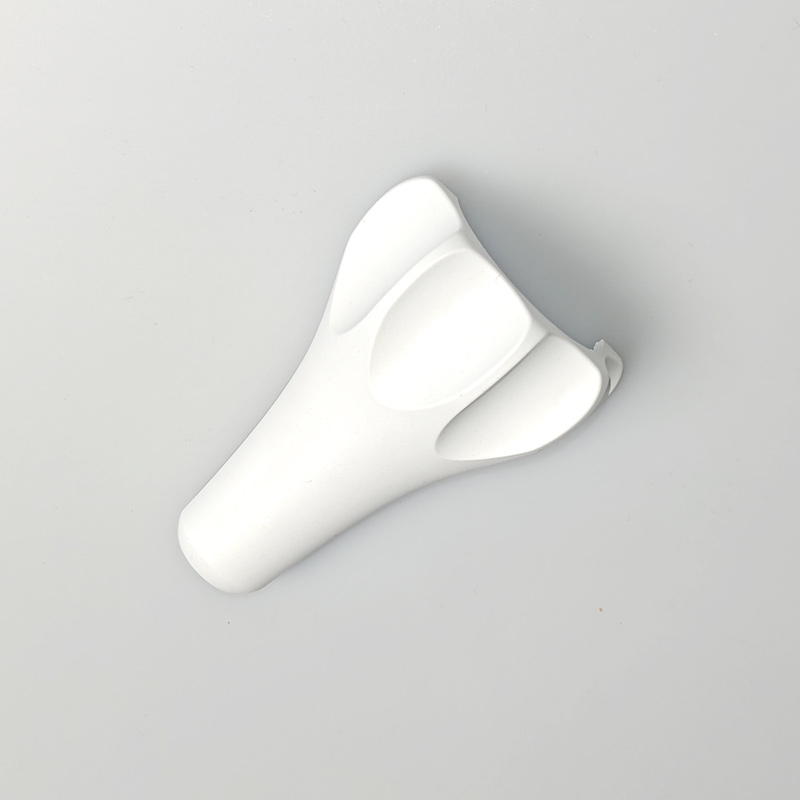
The trumpet profile is comfortable and it is also a moulding challenge in miniature. The section deepens from the narrow stem to the wide skirt, and that transition is where the shrinkage concentrates. An uneven transition leaves the skirt oval or pulls the stem off-axis, and on an instrument where the knob drives a mechanism, an off-axis stem is a functional defect, not a cosmetic one.
Draft angles and ejection are worked out together for the same reason. The deep skirt grips the core, and a knob this size has no place to hide ejector marks, so the ejection layout pushes on the hidden inner face and the surface finish is held on the outer one.
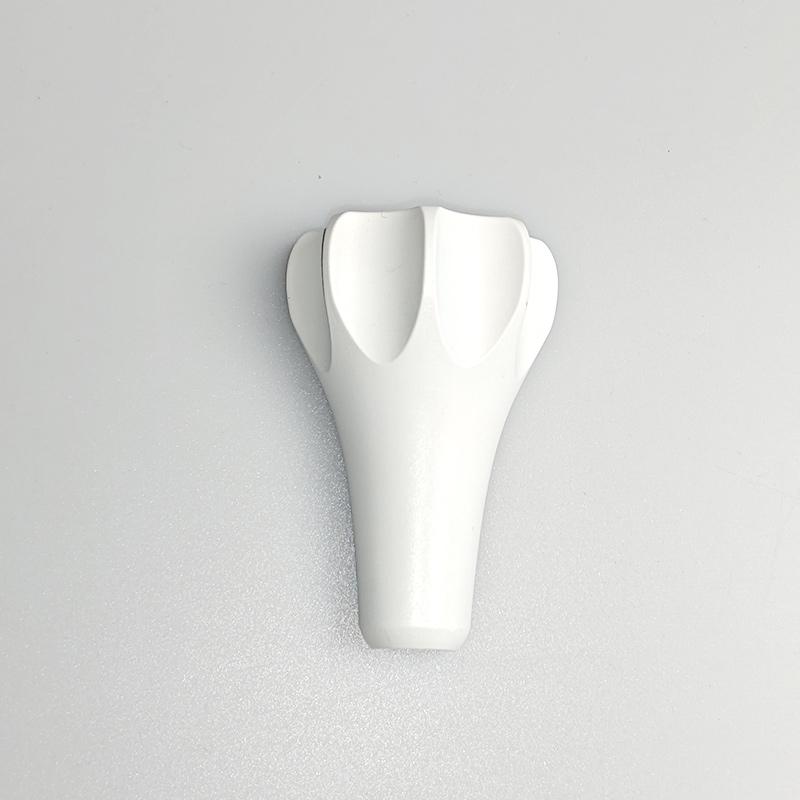
The front face. The recesses at the wide end give the fingers a place to roll the knob without slipping.
The Finger Recesses
The scalloped recesses at the wide end are where the surgeon’s fingers actually sit. Their size and spacing are ergonomics, and their moulding is straightforward geometry: the recesses are formed directly by the cavity, so they repeat exactly. What has to be watched is the wall between adjacent recesses, which thins as the scallops deepen. Too deep and the webs between them sink or warp; the depth is tuned so the grip stays comfortable and the webs stay sound.
Because the knob is often operated with a gloved hand, the recess shape was checked against glove geometry rather than a bare thumb. That is a detail to confirm with the customer early, because it changes the cavity, not just the drawing.
The outer surface. The flare is smooth and seam-free where the hand travels over it.
Internal Thread on a Small Part
The internal thread stack under the skirt is the functional heart of the knob. Thread form, depth and concentricity to the outer profile decide how the closing stroke feels through the fingers. An internal thread on a part this size also decides the tooling: the core either unscrews, collapses or uses a jump-off thread form, and that choice fixes both the tool cost and the cycle time.
Concentricity gets particular attention. If the thread runs slightly off the outer axis, the knob turns with a wobble that reads immediately as poor quality in the hand. The tool is built so the thread and the outer form are cut in register, and concentricity is checked on every lot rather than sampled.
The base. Clip and guide features inside the skirt mate with the instrument body at assembly.
Clip Fit to the Instrument
The clip features inside the skirt snap the knob onto the operating mechanism, and their positions come from the instrument assembly, not from the knob drawing alone. A knob that clips in slightly off-angle turns roughly or jams at the end of travel, so we build the clip geometry against the actual mechanism drawing and check the fit with the mating parts before release.
What Gets Checked Before Shipping
Thread form and concentricity, gauged with the mating mechanism. Clip engagement and turning torque through the full stroke, sampled across the lot. Dimensional report on the skirt and stem axes. Surface and colour against the approved master, since the knob is one of the few parts the user’s fingers rest on continuously.
Information to Confirm Before Starting a Medical Knob Project
The mechanism drawing, including thread form and stroke, since the knob drives it directly.
Resin specification and the sterilization or cleaning exposure the knob will see.
Whether the knob is operated gloved or bare, which sets the recess geometry.
Turning torque target and end-of-travel feel, ideally with a reference sample.
Annual volumes, since a disposable instrument runs knob volumes that justify multi-cavity tools.
Kunshan Maifeng Precision Industry Co., Ltd. reviews medical instrument component designs before quoting, builds the injection molds in house, and molds single-color and dual-color parts on 36 machines from 90 to 700 tons. Send us the mechanism drawing and the resin specification, and we will come back with a feasibility comment and a tooling proposal.
Company Profile
About Us
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 90 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.












 English
 Chinese



