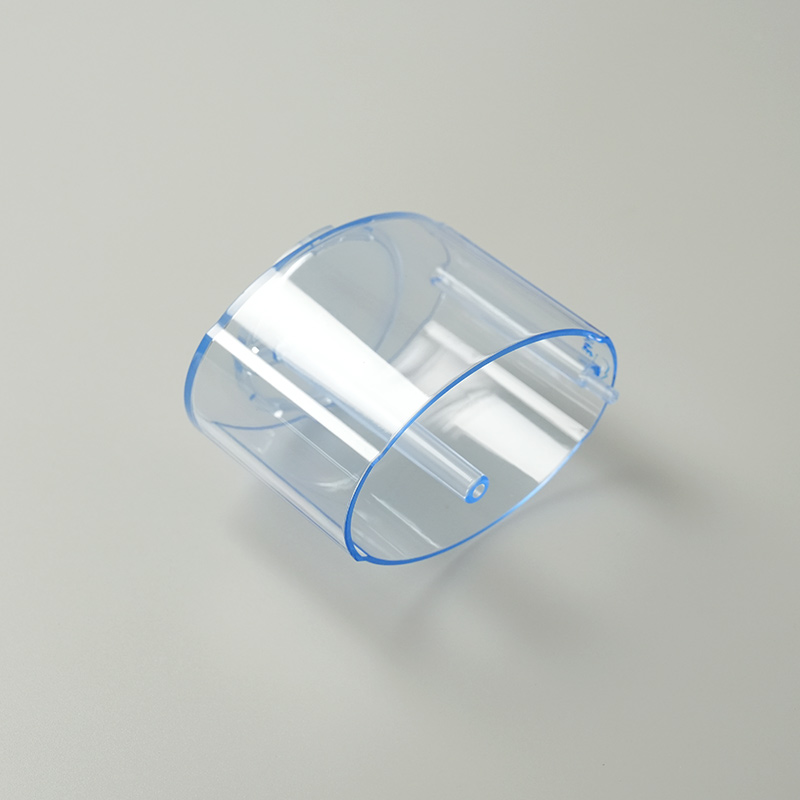
This transparent water guide tube for electric nasal irrigators is moulded in one shot as a cylindrical wall, a closed floor and a slim central flow tube blended into the floor with a radius. The bore of the tube sets the flow rate, and the clear wall lets the user watch water level and flow directly. The mold is gated so the flow front reaches the rim evenly and no weld line crosses the field of view, and the rim is polished at the parting line because the lid seals there. Available in clear PP, SAN or PMMA, each with a different stiffness and shrink trade-off.
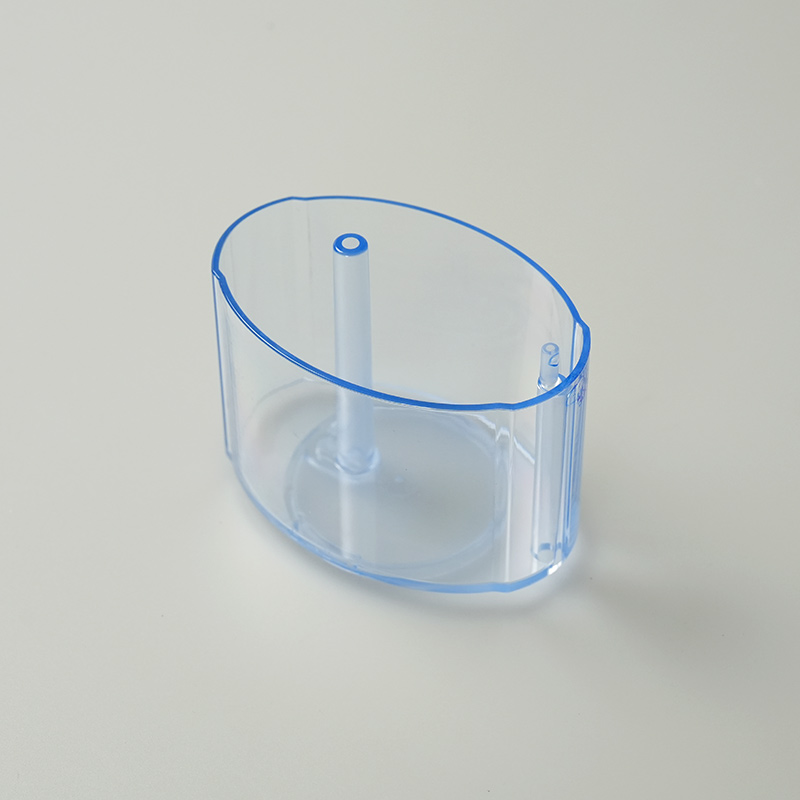
central flow tube moulded integrally with the floor and blended with a radius to spread pump load
gate layout keeps weld lines out of the visible wall and low where the reservoir hides them
rim polished at the parting line because the lid seals on it and flash would show immediately
The water guide tube sits inside an electric nasal irrigator, directly above the pump. Water climbs the central tube, crosses the rim and reaches the nozzle, and because the wall is clear, the user can see the water level and the flow at the same time.
The part is a single moulding: a cylindrical wall, a floor that closes the bottom, and a slim tube standing at the centre of the floor. One material, one shot. The rest of this page covers how we keep a tall thin tube straight and the wall optically clean.
Clear cylindrical water guide with the central flow tube standing from the floor.
The Central Flow Guide Tube
The tube is the functional core of the part. It rises from the floor at the centreline, open at the top, and its bore sets the flow rate. A tube this slim inside a deep cavity is really a second core; the mold cools it from the inside, and if that cooling is uneven the tube leans and the wall around it goes thick on one side, thin on the other.
The base of the tube is where stress collects. We blend the tube into the floor with a radius instead of a sharp corner, which spreads the load when the pump pushes water up and keeps the flow front from stalling at the junction during filling.
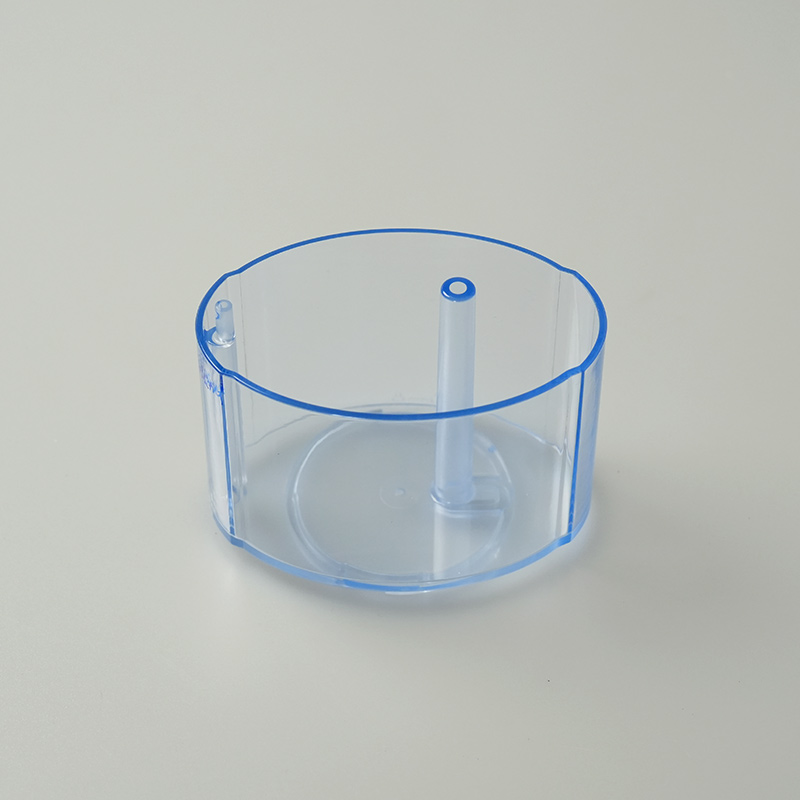
Top view of the water guide showing the open tube bore and the surrounding rim.
Keeping the Wall Optically Clean
Transparency punishes every molding sin. Black specks, flow marks, haze near the gate, weld lines across the rim — all of them show. The part is gated so the flow front reaches the rim evenly and no two fronts meet in the field of view; where a weld line is unavoidable, it is placed low on the wall where the reservoir hides it.
Drying the resin before molding is not optional. Moisture in transparent resin turns into splay, and splay on a part this clear is scrap. The machines run with the hopper dryer on, and the first shots of every shift are held against a light to check for streaks.
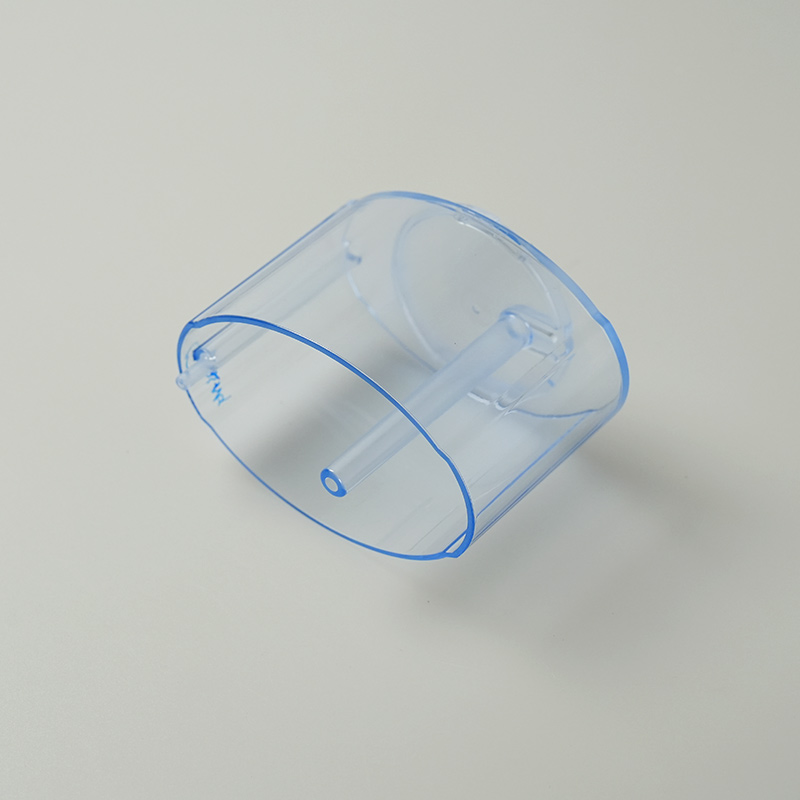
Side view showing the rim edge and the open tip of the central tube.
Rim, Parting Line and Ejection
The rim splits at its top edge. That is the simplest parting line, but it puts the parting line on the visible rim, so the tool steel there is polished and the shut-off is tight; a hair of flash on a clear rim shows from a metre away. The customer’s lid seals on this rim, so roundness matters as much as looks.
Ejecting a deep clear cup without marking it takes stripper push over a wide ring, not pins jabbing the floor. The floor is thickened slightly where it lands on the ejection face. Draft is generous on the outside wall, because transparent surfaces scratch when they drag.
From the Mold to the Packing Bench
Take-out is where a clear part is either protected or ruined. The robot grips the cup on the outside wall with a wide, soft-faced gripper, never on the rim, and lifts it straight off the core so the wall does not drag. Parts land on the conveyor already spaced out, which gives the operator time to look at each one before it reaches the bench.
The bench is the last place a streak can be caught. Every cup is held against the light and turned through a full rotation, which is the only reliable way to see splay, a cold slug or a flow mark on a clear wall. A part that passes goes into the tray open side up, with the tube standing free; a part that fails goes into the red bin, not back into the tray.
Take-out, bench check and packing: the robot lifting a clear cup off the core, the conveyor carrying it to the bench, and the operator turning each water guide against the light before it is set into the tray.
Resin Options for a Clear Waterway
Clear PP, SAN and PMMA all appear in machines like this. PP is the toughest and handles saline without complaint, but it has the lowest stiffness and the highest shrink, so the tube is hardest to keep straight in PP. PMMA is stiff and crystal clear but brittle at the rim. SAN sits between. The choice belongs to the customer; our job is to say what each one will cost in cycle time and scrap rate before the steel is cut.
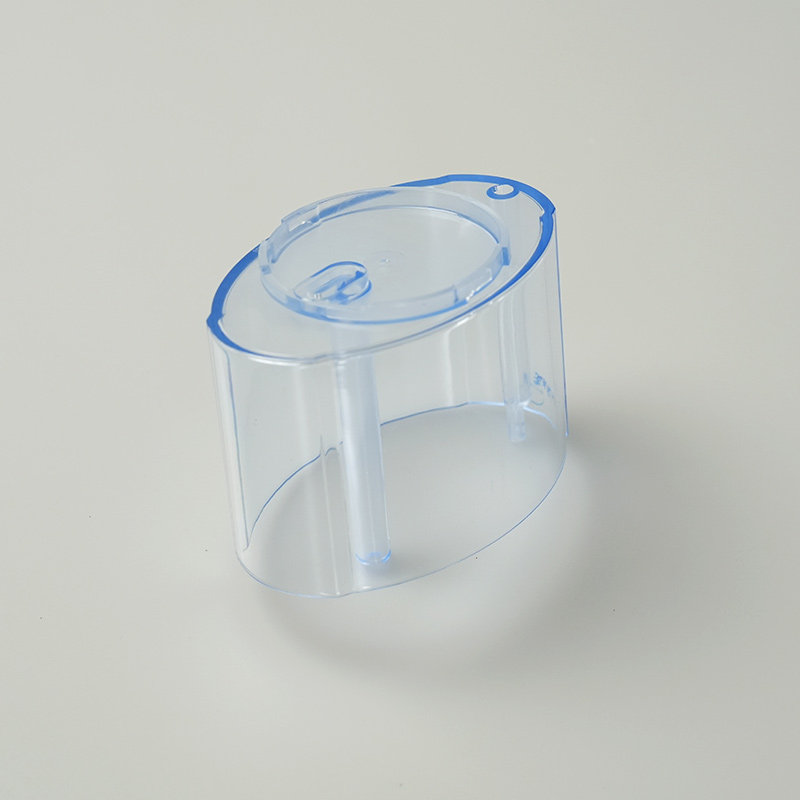
Tilted view of the water guide showing the tube blended into the floor.Side view of the finished water guide showing the smooth outer wall and even rim.
Information to Confirm Before Starting a Transparent Waterway Part Project
The bore and height of the central tube, since they set the flow rate and the core cooling.
The resin, or at least the shortlist, because PP, SAN and PMMA mold very differently.
Whether the part needs to read as an optical component or only as a functional window.
The lid or rim interface, including the seal type and the roundness it demands.
Volume expectation, which decides gate type and whether a hot runner pays for itself.
Kunshan Maifeng Precision Industry Co., Ltd. reviews transparent waterway part designs before quoting, builds the injection molds in house, and molds single-color and dual-color parts on 36 machines from 40 to 700 tons. Send us the 3D model of the tube and the flow specification, and we will come back with a feasibility comment and a tooling proposal.
Contact Us
Lucie — Kunshan Maifeng Precision Industry Co., Ltd.
Custom Mold. Precision Injection Molding. Reliable Production. Send us the 3D model of the tube and the flow specification, and we will come back with a feasibility comment and a tooling proposal.
Company Profile
About Us
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 40 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.











 English
 Chinese



