This replacement sliding lid for sports tumblers is molded in smoky-transparent polycarbonate with the slide mechanism built into the top surface. A moulded closure rides in a track with detents at both ends of travel, opening and closing a star-shaped drinking aperture that meters flow instead of flooding it. A silicone gasket sits in an undercut groove under the closure for a leak-proof seal, and the snap skirt is built to the tumbler rim it serves. Slide action, seal integrity and tumbler fit are verified on finished assemblies before shipping. Slide layout, tint and skirt geometry can be adapted to a customer design.
moulded slide track with detents at both ends of travel, so the closure does not drift open
star-shaped aperture meters the flow, and the gasket groove keeps the seal when closed
skirt geometry built to the actual tumbler rim, not to a generic diameter
A sliding tumbler lid gets more use than almost any other moulded part on a drinkware line. It is opened and closed dozens of times a day, it sits over liquid that is sometimes hot, and it is expected to survive the dishwasher and the occasional drop on a hard floor. The lid shown here is a replacement sliding lid in smoky-transparent PC, moulded with its slide mechanism built into the top surface.
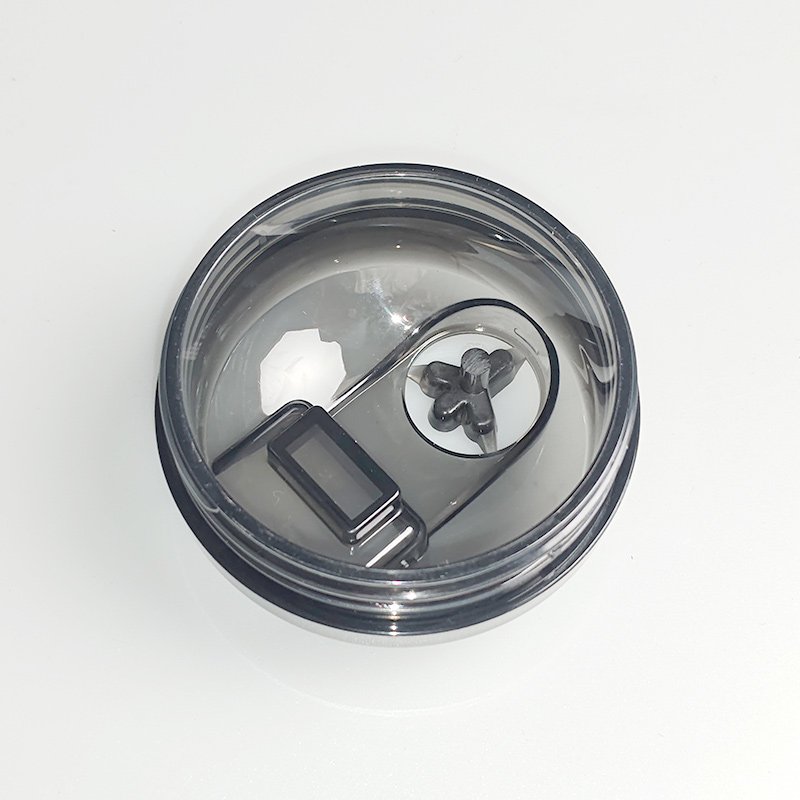
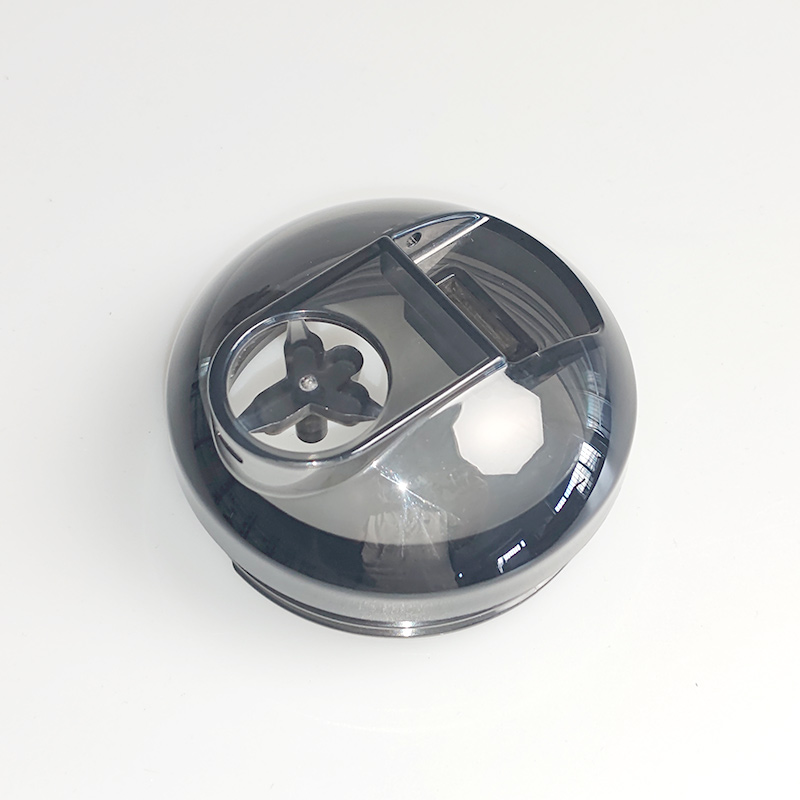
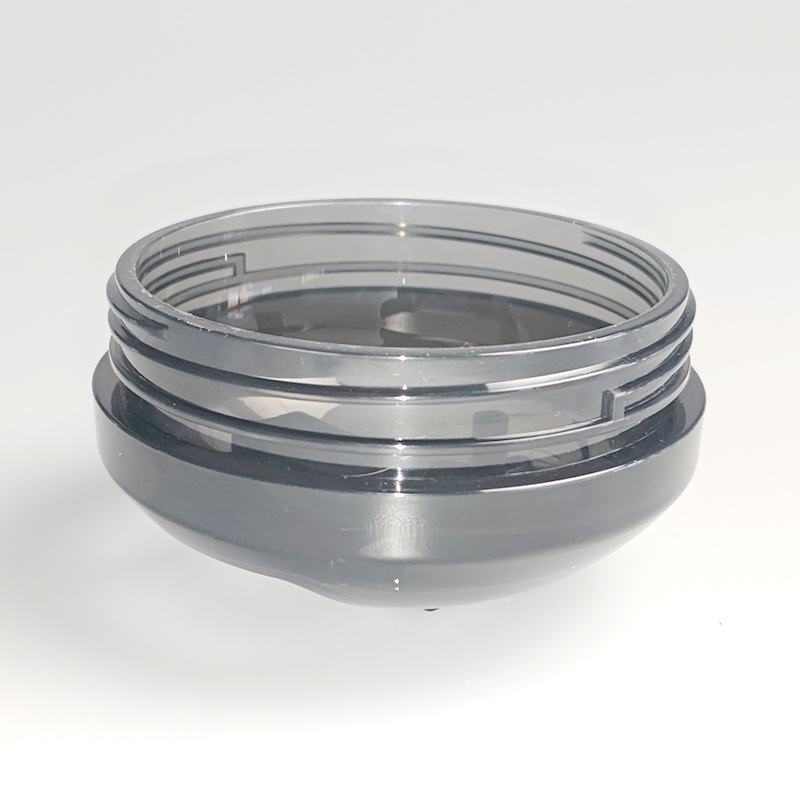
The three views show the working face, the closed top with the slide button, and the underside with the threaded skirt. The slide opens and closes a drinking aperture in the top; a silicone gasket under the closure keeps the seal when it is shut; and the skirt snaps down onto the tumbler rim.
The working face. The slide button moves across the track to open and close the star-shaped drinking aperture.
How the Slide Mechanism Works
The closure is a moulded plate riding in a track formed in the lid top. In the closed position it covers the drinking aperture completely; slid across, it lines its own opening up with the aperture and the drink flows. The star-shaped hole in the closure is not decorative. A round hole floods; a star profile meters the flow and gives the liquid somewhere to go when the tumbler tips toward the mouth.
The slide has to feel defined at both ends of its travel. That feel comes from detents moulded into the track: small bumps the closure rides over and settles behind at each end of travel. Without them the closure drifts, and a lid that drifts open in a bag is a lid that returns for a refund.
Closed position. The closure sits flush in the recess so nothing stands proud of the lid top.
Moulding the Track and the Sealing Face
The slide track is the hardest geometry in this part. Its walls are small, its tolerances are tight, and the closure has to glide in it without rocking. Any flash along the track edges shows up immediately as a sticky or gritty slide, so the parting line around the track is planned rather than wherever the tool happens to split.
The sealing face around the aperture needs the opposite treatment. Where the track wants a hard, slick surface, the gasket seat wants a clean flat land for the silicone to press against. A land that is too narrow pinches the gasket; too wide and the gasket lifts at the edges of the aperture. Both faces are on the same moulded surface, so both are controlled by the same tool steel.
Smoky-Transparent PC
PC earns its place here. It is transparent, so the user can see how much drink is left through the lid, it takes impact without cracking, and it handles dishwasher cycles far better than clear styrenics, which craze and cloud after a few months. The smoky tint is chosen in the compound rather than sprayed on, so the colour is consistent through the wall thickness and does not wear.
The trade is that PC wants careful drying before moulding. Moisture in the resin shows up as streaks and bubbles in a transparent part, which would be invisible in an opaque lid of the same design. Drying to spec before every run is part of the process, not an option.
The underside. The skirt grips the tumbler rim and the groove takes the silicone gasket that seals the assembly.
The Fit to the Tumbler
The skirt is the part that has to agree with somebody else’s tumbler. As a replacement lid, its rim geometry is built to the tumbler it serves, and the tolerance on that diameter is what decides between a lid that seats with a clean snap and one that sits loose or refuses to go on. This is why we ask for the tumbler rim drawing or a sample before quoting a replacement lid, not just the old lid.
What Gets Checked Before Shipping
Slide action, cycled by hand across a sample from each lot to catch gritty spots. Detent feel at both ends of travel. Seal integrity with the gasket fitted, checked with water rather than assumed. Fit onto the actual tumbler rim, and drop performance of the closed lid on a filled tumbler where the customer specification calls for it.
Information to Confirm Before Starting a Replacement Lid Project
The tumbler rim drawing or a sample, since the skirt geometry and tolerance are built to it.
Whether the gasket is supplied fitted or shipped separately for the customer to install.
Slide travel layout, aperture shape and whether the closure should also cover a straw slot.
Resin and tint specification, and any dishwasher or food-contact requirement for the destination market.
Annual volumes, which decide whether a single-cavity tool or a multi-cavity family tool makes sense.
Kunshan Maifeng Precision Industry Co., Ltd. reviews drinkware lid designs before quoting, builds the injection molds in house, and molds single-color and dual-color parts on 36 machines from 90 to 700 tons. Send us the tumbler rim drawing and the slide layout you want, and we will come back with a feasibility comment and a tooling proposal.
Company Profile
About Us
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 90 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.












 English
 Chinese



