Router Plastic Antenna, External Injection Antenna for Wireless Router
This router antenna shell is a long tapered body moulded in one piece from a white resin. The open base carries a moulded collar and bore that locate the connector assembly and set the pivot axis, so the antenna holds the angle it is left at. Wall thickness around the radiating element is treated as part of the RF design, and no conductive filler is used in the resin. We can adjust the taper, base geometry, colour and surface finish to a customer connector drawing.
long tapered shell moulded straight, with wall and cooling balanced against bow
moulded collar and bore hold the connector fit and set a consistent pivot feel
resin free of conductive filler so the shell does not screen the radiating element
The plastic body of a router antenna is not the part that radiates. The radiating element is inside it, and the shell has one job: hold that element straight, let it pivot to the angle the user wants, and look acceptable sitting on a desk for a couple of years. Getting that wrong does not show up as a cosmetic problem. It shows up as an antenna that will not stay where it is pointed, or one that will not screw onto the connector without force.
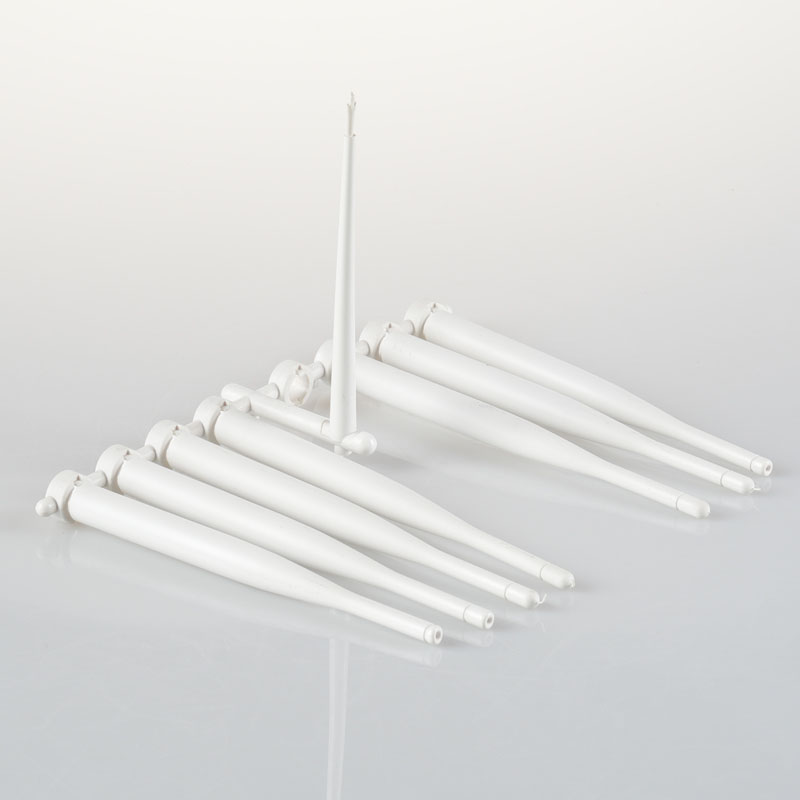
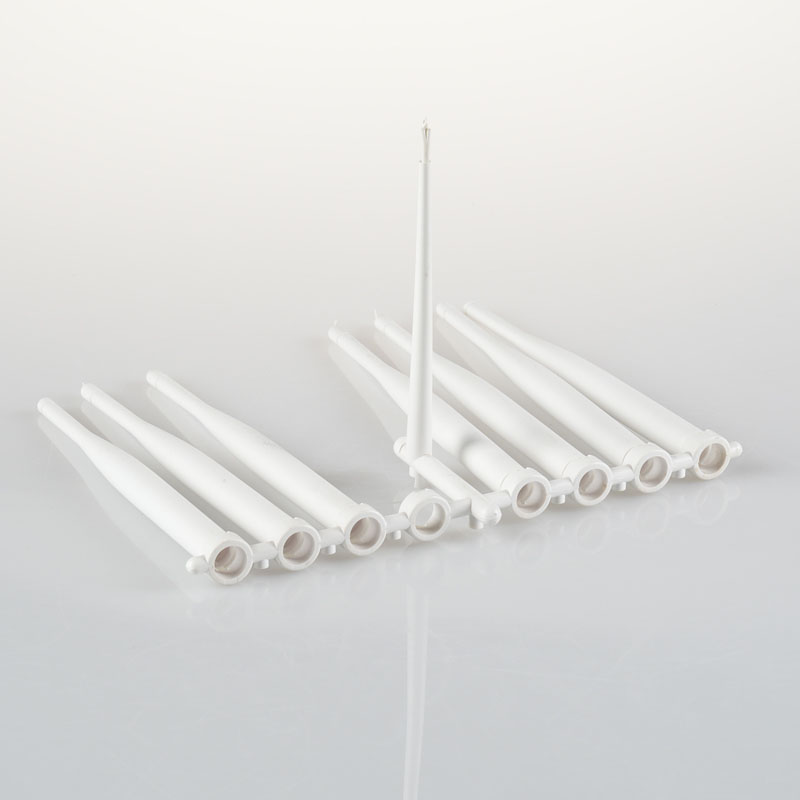
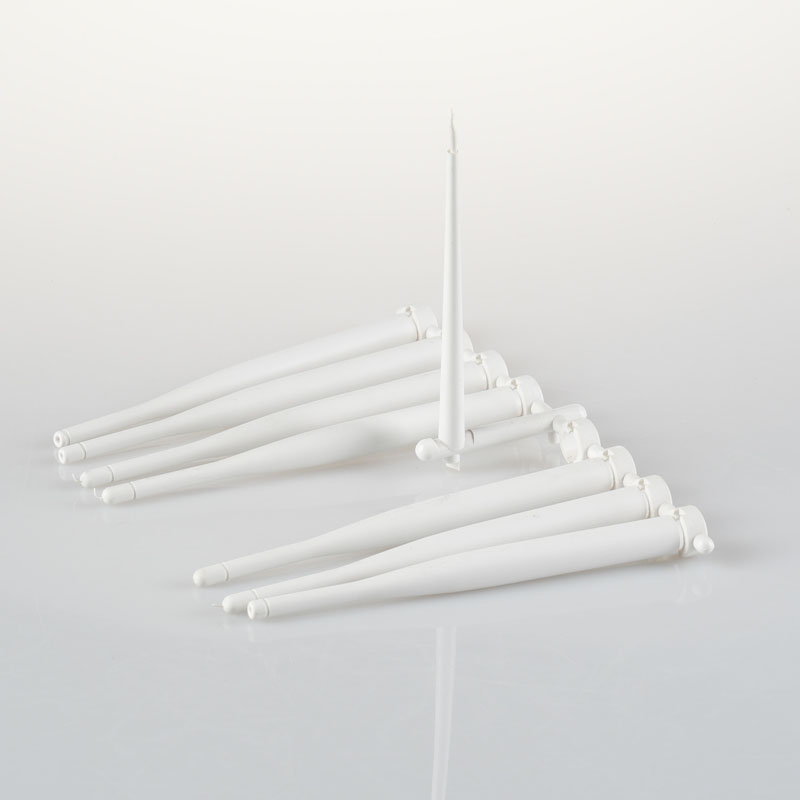
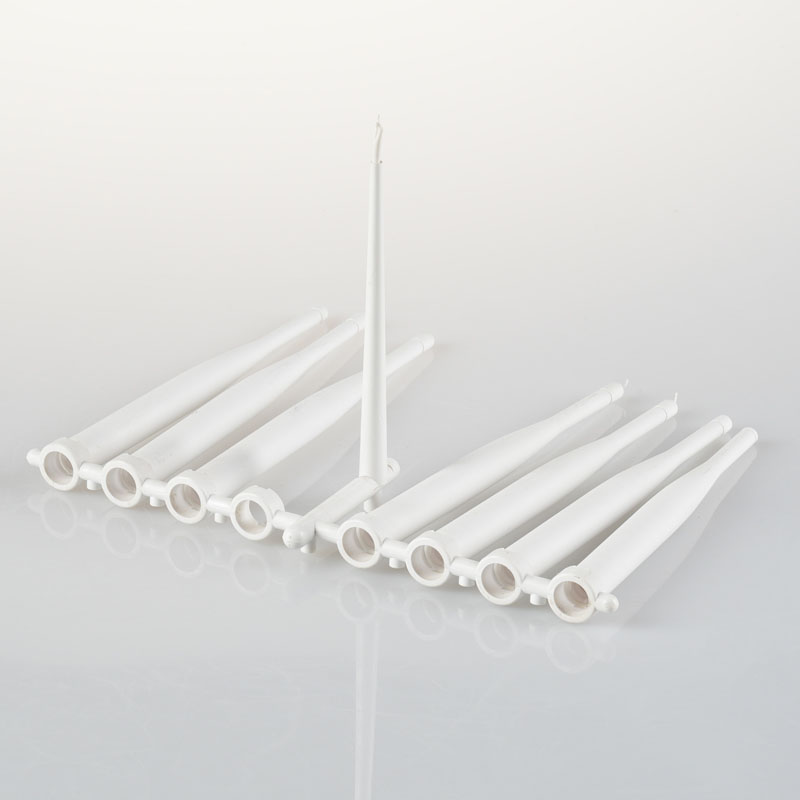
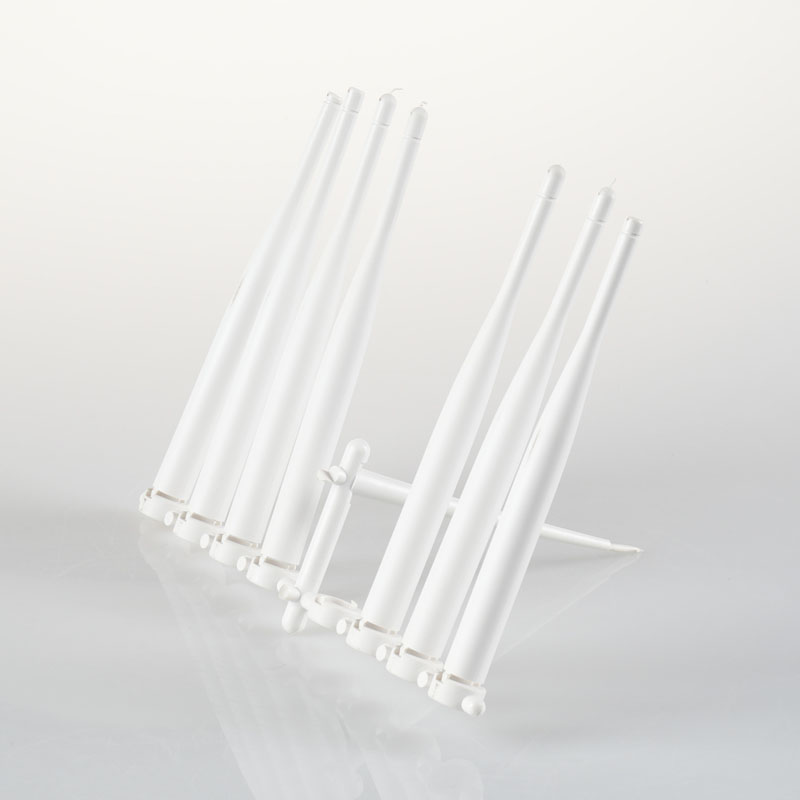
The shells in these photographs are moulded in one piece from a white resin, tapered from a wide base to a narrow tip. The base is open, with a moulded collar inside that locates the connector assembly and carries the pivot. Five shells are shown from several angles, including the open base, which is where most of the dimensional work on this part actually sits.
One shell standing upright. The taper is continuous from base to tip with no step or witness line along the length.
A Long, Thin, Tapered Shell
Length is the problem here. The shell is many times longer than it is wide, and any difference in shrinkage between one side and the other comes out as a bow. A bowed antenna looks wrong on a finished router, and past a certain amount it will not seat in the base without being pushed. The usual countermeasures apply: uniform wall, balanced cooling around the cavity, and enough cooling time that the part has finished moving before it is ejected.
The taper helps rather than hinders. A constant wall on a cone ejects more cleanly than a constant wall on a cylinder of the same length, and the narrowing section gives the tip somewhere to go. What needs watching is the transition into the base, where the wall thickens to carry the collar. That is the region where sink marks would appear on a gloss surface, and it is also the region the user’s fingers cover when adjusting the antenna.
The open bases. The bore and the internal collar locate the connector assembly and set the pivot.
The Base, the Bore and the Pivot
Everything the user interacts with happens at the base. The bore has to accept the connector with a defined fit: loose enough to assemble, tight enough that there is no play. The internal collar sets the axis the antenna pivots on, and the friction in that pivot decides whether the shell stays at the angle it was left at. Too little friction and the antenna flops down; too much and the user twists the whole router instead.
That friction is set by geometry, not by luck. Contact area, the surface finish of the mating faces and the interference designed into the parts all contribute. Because the collar is moulded rather than machined, its dimensions come from the tool and repeat shot to shot, which is what keeps a batch of antennas feeling the same in the hand.
Collar detail. The bore wall is moulded to a defined thickness so the connector fit stays consistent.
Resin Choice and the Radio
Anything conductive in the shell works against the antenna. Carbon-filled resins and some metallic pigments screen radio frequencies and are simply not options here, even though either might be the obvious choice for a matching black or grey part elsewhere on the product. The filler has to be inert as far as the radio is concerned.
Wall thickness around the radiating element matters for a different reason. The element is tuned with the shell in place, so the wall is part of the RF design rather than just a mechanical boundary. Changing it mid-programme means retuning, which is a good argument for fixing the wall before the tool is cut rather than adjusting it afterwards.
A set of shells. The colour and gloss match across the batch, which is what a visible external part needs.
What Gets Checked on an Antenna Shell
Straightness over the full length, since that is the defect most likely to appear. Bore diameter and collar position, checked with the actual connector assembly rather than a gauge alone. Pivot feel, assessed by hand across a sample from the lot. Colour and gloss against the approved master. Where the customer supplies the internal element, a transmission check on assembled units confirms the shell is not screening the radio.
Information to Confirm Before Starting an Antenna Shell Project
The connector assembly drawing, since the bore, collar and pivot geometry all depend on it.
Resin and colour specification, with confirmation that no conductive filler is present.
Pivot friction target or a reference sample to match the feel against.
Whether the internal element is supplied by the customer or sourced alongside the moulding.
Annual volume and the number of colours required, which decide the cavity count and tooling plan.
Kunshan Maifeng Precision Industry Co., Ltd. reviews antenna and communication part designs before quoting, builds the injection molds in house, and moulds single-color and dual-color parts on 36 machines from 90 to 700 tons. Send us the connector drawing and the resin specification, and we will come back with a feasibility comment and a tooling proposal.
Company Profile
About Us
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 90 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.












 English
 Chinese



