Sports Bottle Accessory Flip Spout Lid with Carry Handle
This sports bottle lid combines a flip-top drinking spout and an integrated carry loop in one moulded piece. The flip top runs on a living hinge gated to flow across the hinge zone for cycle life, and it locks open and closed. The spout seals onto a soft plug that conforms to the bore, and the vent and drink openings are positioned so the bottle pours without glugging. The carry loop is widest at the top where a full bottle hangs, with the root region packed deliberately to take the load. Hinge life, seal integrity and loop strength are verified on finished assemblies. Spout layout and colour can be adapted to a customer design.
living hinge gated to flow across it, so the flip top survives far past its rating
soft plug seal conforms to the spout bore instead of relying on hard-to-hard contact
carry loop moulded integrally with its widest section where a full bottle hangs
A carry-handle lid travels more than the bottle does. It gets slung over a wrist, hung from a hook, and flipped open one-handed while the other hand is busy. The lid shown here is a replacement flip-spout lid in a dark matte finish, with the carry loop moulded as part of the same piece and a sealed spout under the flip top.
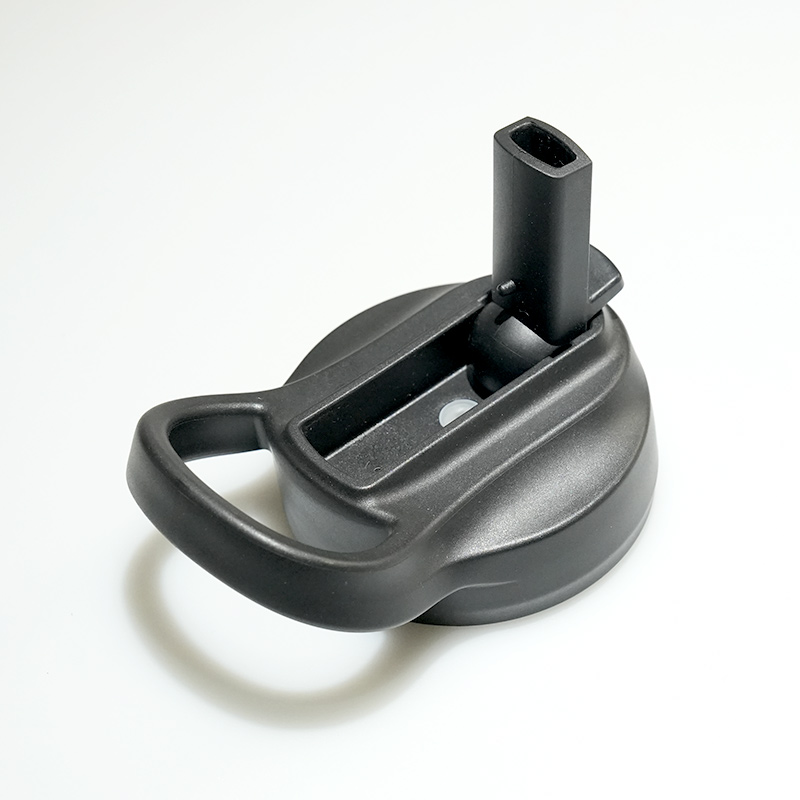
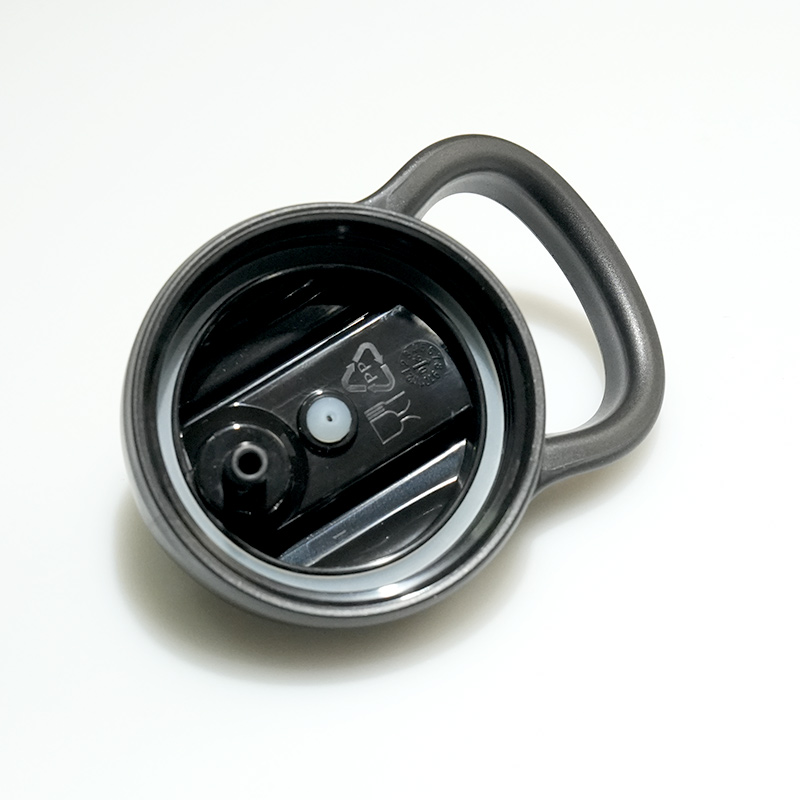
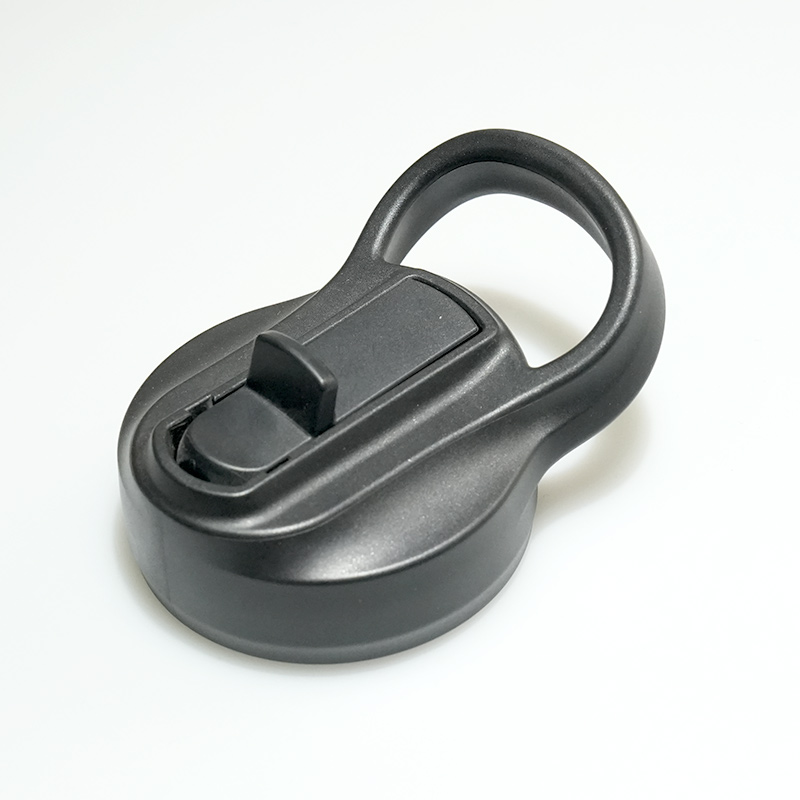
Three views show the spout open, the inside with its sealing features, and the lid closed with the loop standing up. The flip top works on a moulded hinge, the spout closes onto a soft seal, and the underside carries the geometry that locks the lid to the bottle neck.
Spout open. The square spout stands up on its moulded hinge and locks open for drinking.
The Living Hinge
The flip top works on a living hinge: a thin, controlled section of the same moulded piece that flexes every time the lid opens and closes. No pin, no separate spring. The hinge cross-section is the whole design, thick enough to carry the load of the spout standing up, thin enough to flex thousands of times without whitening or cracking.
Hinges are decided at the tooling stage and they are sensitive to processing. Melt temperature, packing and the direction of flow across the hinge all affect its life, so the hinge zone is gated to flow across it, never along it. A lid that opens smoothly for a week and snaps at the hinge in a month was moulded wrong, not designed wrong, and the difference shows up in process control.
The inside. The sealing plug seats into the spout bore, and the moulded symbols identify the vent and drink positions.
Sealing the Spout
The closed lid has to keep a bag-pressed bottle from weeping and keep the drink inside during a bumpy commute. The sealing plug moulded on the underside seats into the spout bore, and the fit is set by geometry rather than by force: the plug flexes in, seats, and holds. Where the seal matters most, a soft plug material is used against the rigid spout so the two conform instead of relying on perfect hard-to-hard contact.
The vent position matters as much as the drink position. A lid that seals perfectly on both will glug and splash, because air has to enter as liquid leaves. The moulded symbols on the inside identify which opening does what, and the relationship between the two is part of the flow design, not an afterthought.
Closed, with the loop up. The loop is moulded into the same piece as the lid body and takes the weight of a full bottle.
The Carry Loop
The loop is moulded integrally because a pinned or welded loop is one more part to fail. Its cross-section is widest at the top, where a full bottle hangs its weight, and narrows toward the root, spreading the stress instead of concentrating it at the joint. The root region is also the place where the moulding flow has to arrive last and pack fully, which is why the gate layout feeds it deliberately.
The loop has to stand up when in use and lie flat enough not to snag when the lid is stored or washed. That action is a spring geometry of its own, tuned by the root thickness, and it shares the living-hinge logic of the flip top.
What Gets Checked Before Shipping
Hinge cycle life, opened and closed on a fixture well past the rating. Seal integrity with the lid closed on a filled bottle, tipped and squeezed. Loop strength, hung with a load well above a full bottle’s weight. Spout lock in both open and closed positions, and the fit of the underside geometry to the actual bottle neck.
Information to Confirm Before Starting a Flip Lid Project
The bottle neck drawing, since the underside locking geometry is built to it.
Spout bore and seal requirement, including whether a straw must pass through.
Resin specification and food-contact requirements for the destination market.
Whether the seal is rigid-to-rigid or uses a soft plug, and who supplies the soft part.
Annual volume, which decides whether the hinge and loop justify a dedicated single-cavity tool.
Kunshan Maifeng Precision Industry Co., Ltd. reviews drinkware closure designs before quoting, builds the injection molds in house, and molds single-color and dual-color parts on 36 machines from 90 to 700 tons. Send us the bottle neck drawing and the spout layout, and we will come back with a feasibility comment and a tooling proposal.
Company Profile
About Us
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 90 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.












 English
 Chinese



