Integrated Linked Flip Lid Thermos Straw Accessory with Handle
This thermos straw lid links its outer cover and built-in spout through a moulded cam relationship: flipping the cover lifts the spout through a defined path and seats it again on closing, one motion, no second step. The cap is two-color injection molded, with the sealing body, soft carry handle and translucent hinge cover formed as three resins in coordinated shots, so there are no glued joints or clip lines to separate in daily washing. Twin bores under the cover, straw and vent, each carry a sealing element tuned to its own duty, and the thread stack is built to the thermos mouth. Linkage wear, hot-water seal and vent behaviour are verified before shipping.
moulded cam link opens cover and spout in one motion and seats them square on closing
three resins in two-color shots: sealing body, soft handle and translucent hinge cover
straw and vent seals engineered separately for pressure head versus bag weeping
Most flip lids need two motions: flip the cover, then find and open the spout underneath. The lid shown here links the two. Opening the outer cover lifts the built-in spout with it, one motion, and closing pushes the spout back into its seat. It is a two-color moulded cap for a thermos, with the carry handle, the cover and the body all formed as separate materials in coordinated shots.
Six photographs cover the cap from every side, including the underside where the twin bores and their sealing features live. The colour split is not decoration: body, handle and translucent cover are different resins chosen for different jobs, and the two-color process is what lets them meet in one piece.
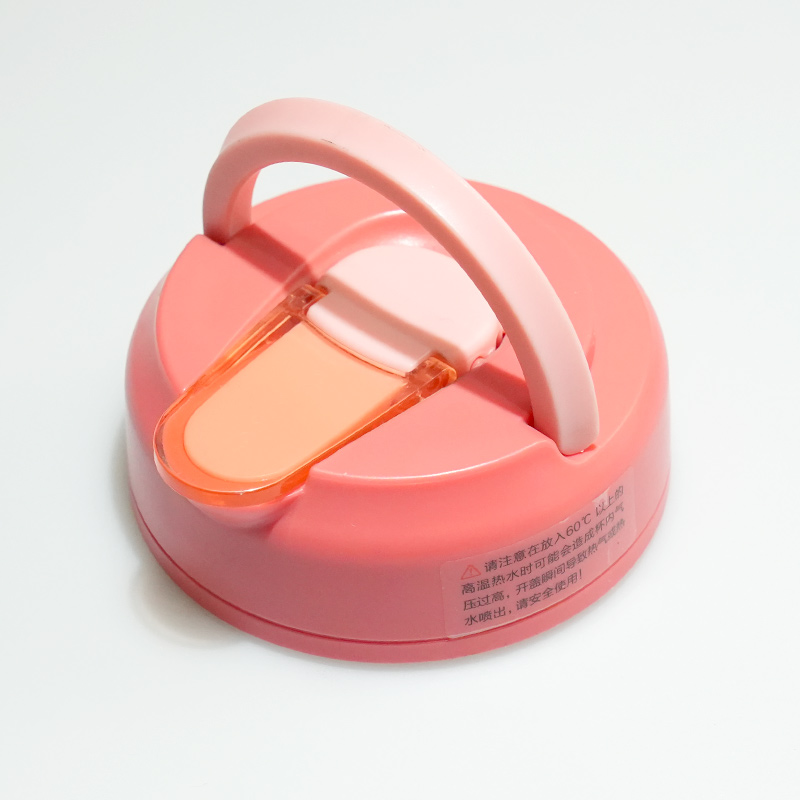
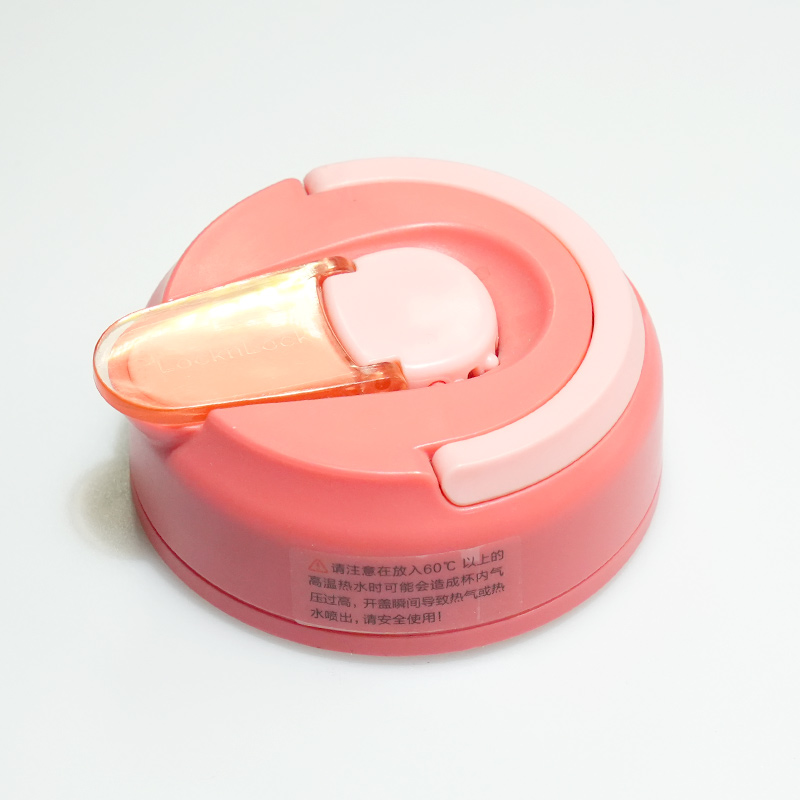
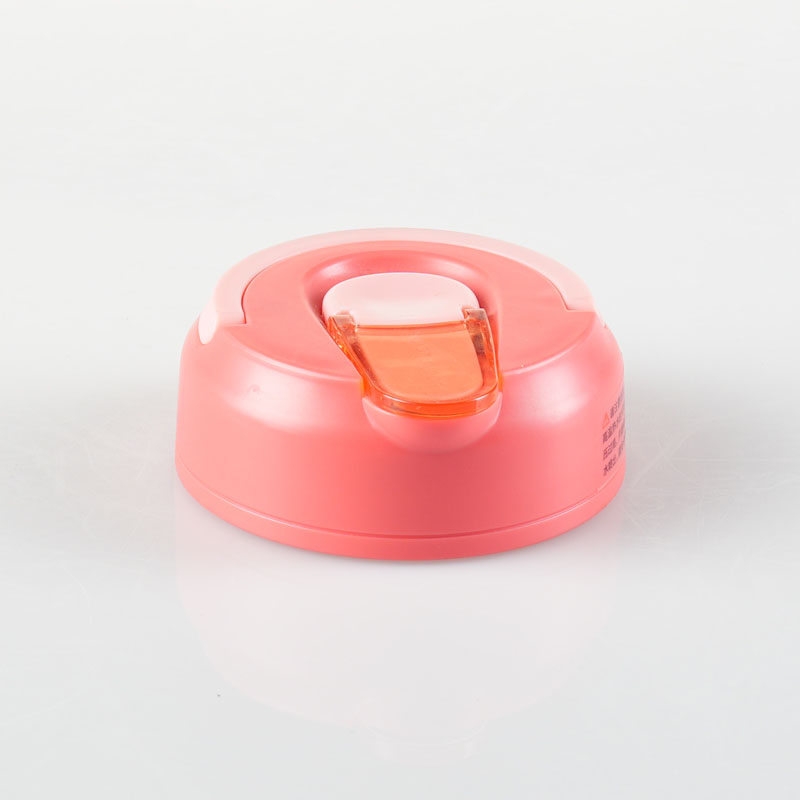
Closed. Body, handle and translucent cover are three resins moulded into one coordinated piece.
The Linked Mechanism
The linkage between cover and spout is a moulded cam relationship, not a separate moving part. The cover’s hinge carries a lobe that rides against the spout’s base, so rotating the cover lifts the spout through a defined path and drops it back onto its seat on closing. The path matters: the spout has to clear the cover aperture without dragging, and seat square enough that its seal works from any angle the user happens to close it.
Cam profiles like this are tuned in the tool, not on paper. Draft, hinge flex and resin shrinkage all shift the actual path a few percent, so the first trials are watched, measured and corrected in the steel before the production window is frozen.
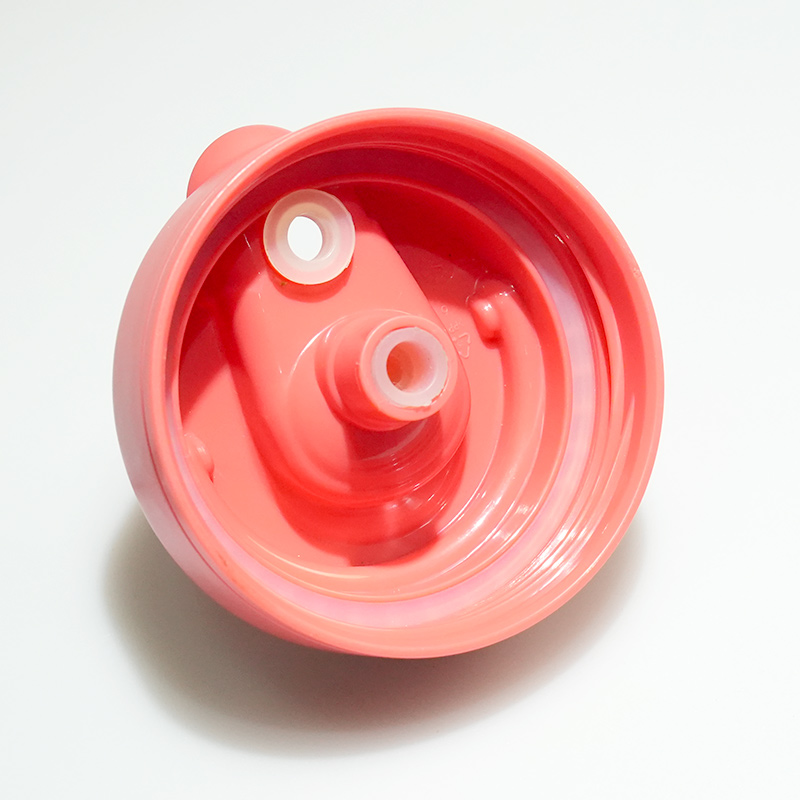
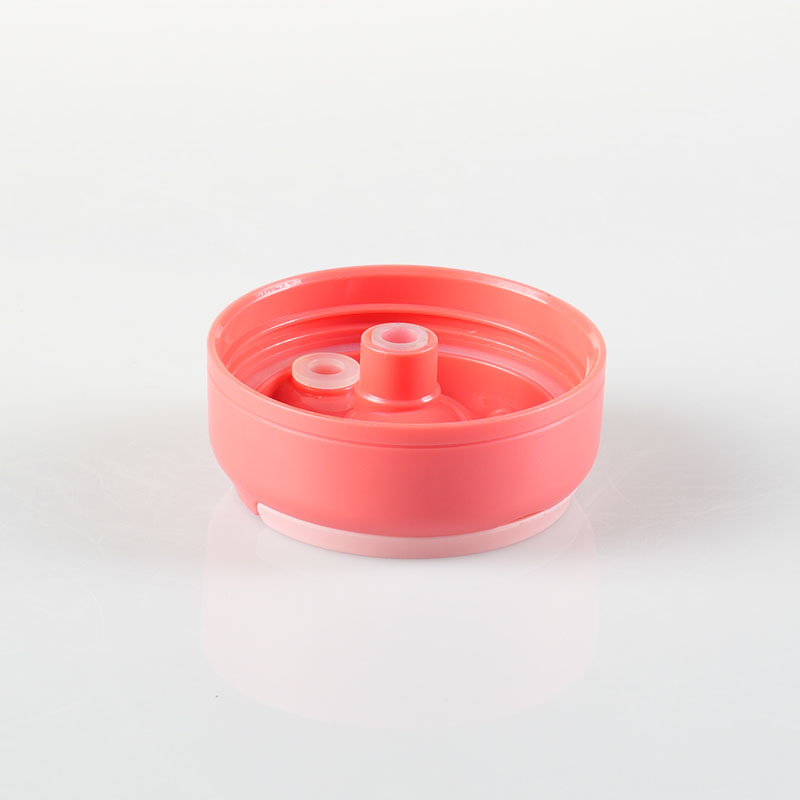
The underside. Twin bores, straw and vent, each with its own soft sealing element.
Twin Bores and the Vent Relationship
Two openings live under the cover: the straw bore and the vent. The straw carries the drink; the vent admits air so the flow stays smooth. Their relationship is flow design, and the sealing elements under each are tuned differently: the straw seal works against liquid head and pressure, the vent seal against weeping in a bag. A single sealing approach for both fails at one or the other, so they are engineered separately even though they sit centimetres apart.
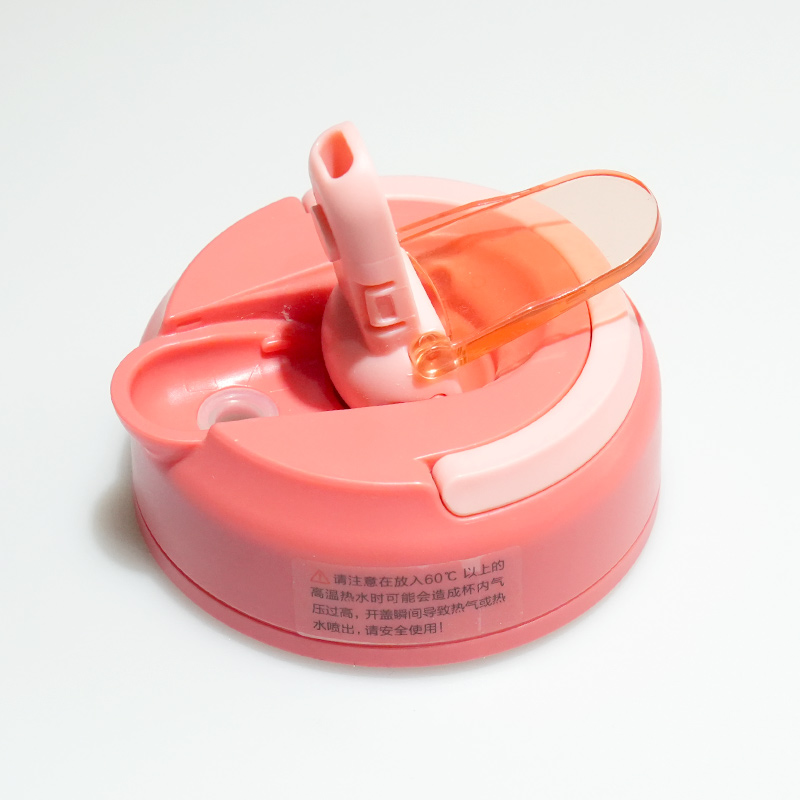
One motion. The cover flips and the spout rises with it through the moulded cam path.
Why Two-Color Instead of Assembly
This cap could be built from moulded parts assembled by hand, and many are. The two-color route costs more in tooling and less in assembly, and it shows up in the product: no glued joints to separate in a hot car, no clip lines across the appearance surfaces, and colour boundaries that stay exactly where the tool put them. For a lid that gets washed daily and handled wet, that difference in durability is the argument.
The translucent cover resin is chosen to be seen through and to take hinge flex; the body resin to seal and to hold the thread; the handle resin to be soft where the hand lands. Three compounds, three shots, one part.
Fully open. The spout stands clear of the cover aperture and locks into drinking position.The thread stack and seal seats, moulded into the base and gauged against the thermos mouth.
What Gets Checked Before Shipping
Linkage action, cycled open and closed past the rating with the cam path watched for wear. Seal under heat on both bores, the vessel laid on its side. Vent behaviour while drinking. Thread torque against the thermos mouth, and colour boundary sharpness between the three materials.
Information to Confirm Before Starting a Linked-Flip Lid Project
The thermos mouth drawing, since thread and seals are built to it.
Drink type, straw versus direct sip, since the twin bores are designed around it.
Whether the linked action is required or two-step operation is acceptable, which changes the tooling cost.
Colour and material specification for all three resins, with masters.
Annual volume, which decides whether two-color tooling pays for itself against assembly.
Kunshan Maifeng Precision Industry Co., Ltd. reviews two-color closure designs before quoting, builds the injection molds in house, and molds single-color and dual-color parts on 36 machines from 90 to 700 tons. Send us the thermos drawing and the operation requirement, and we will come back with a feasibility comment and a tooling proposal.
Company Profile
About Us
Kunshan Maifeng Precision Industry Co., Ltd. (MIF) has an investment of RMB 35 million and an independent factory of more than 5,000 m². The company operates 36 single- and dual-color injection molding machines from 90 to 700 tons, together with more than 50 sets of mold manufacturing and processing equipment. Our service, management and production team includes over 100 people.
Our parent company was established in 2008. We provide product design, mold design and manufacturing, injection molding and product assembly services for custom plastic parts, supporting both domestic and international customers.
1. Product Design Product structure design and optimization based on customer drawings and samples.
2. Mold Design Mold design developed around product geometry, material and production requirements.
3. Mold Manufacturing Machining, polishing, fitting and assembly for custom injection molds.
4. Injection Molding Single- and dual-color injection molding for project and order requirements.
5. Product Assembly Supporting assembly services for molded plastic components.
Custom glossy black PC protective cover for lawn mowers: an open-ring shell with snap clips molded in one shot and a class-A face that survives stones, sun and cleaning.
Custom PC light-diffusion tail light grille for lawn mowers: an even light band, a ribbed outer face, a sealed fixing flange and an optical surface finished to the agreed polish.
Custom clear PC tail light strip for mowers and outdoor equipment: compound curve, uniform wall, polished optical face and colour matched to your chip.
PC+ABS automotive wireless charging housing with an open coil window, four mounting ears and a stiffening rib, molded, inspected and packed for console assembly.
PC lawn mower tail light grille produced through custom mold development, precision injection molding and strict quality control for demanding outdoor applications.
PP handles and plastic parts for a 3rd generation magnetic wall mounted toilet brush, produced at Maifeng Precision through custom mold design, injection molding and careful inspection.
ABS nasal irrigator outer housing produced with custom multi-cavity molds, precision injection molding, careful trimming and dust-free packaging for personal care brands.
ABS nasal irrigator base produced with custom mold design, precision injection molding, strict inspection and dust-free packaging for personal care and medical device assemblies.
No matter what your automotive needs may be, we’re here to help. Contact us today to learn more about our
services and how we can assist you with all of your needs.
ISO 13485-certified medical injection molding in Class 10,000/100,000 cleanrooms: 36 single and dual-color machines, proven medical cases and trusted partners.
One-stop cup and bottle molding: dual-color lids, tea-separation cups and handles, QS food-contact licensed production with proven cases for global brands.
Contact Us
To grow into a top global mold & injection molding supplier
To grow into a top global mold & injection molding supplier, specializing in differentiated custom parts. We focus on structural development, streamlined production and consistent quality supply.












 Chinese
 English



